Daftar Isi
Tile adhesive additive dosing should be specified from the smallest quantity the factory needs to handle reliably, not only from the maximum batch capacity. An additive can be a small part of the total mass while remaining significant to the product's performance. The equipment discussion therefore needs to cover measurement, feeding, transfer, identification and batch records as one material route.
This guide addresses procurement and process verification for powder additives in a dry tile-adhesive line. It does not provide a formulation or prescribe additive percentages. Those depend on the product design and validation work. The aim is to help a buyer communicate the actual dosing range and request evidence that the proposed system can handle it under representative production conditions.
Define the tile adhesive additive dosing range
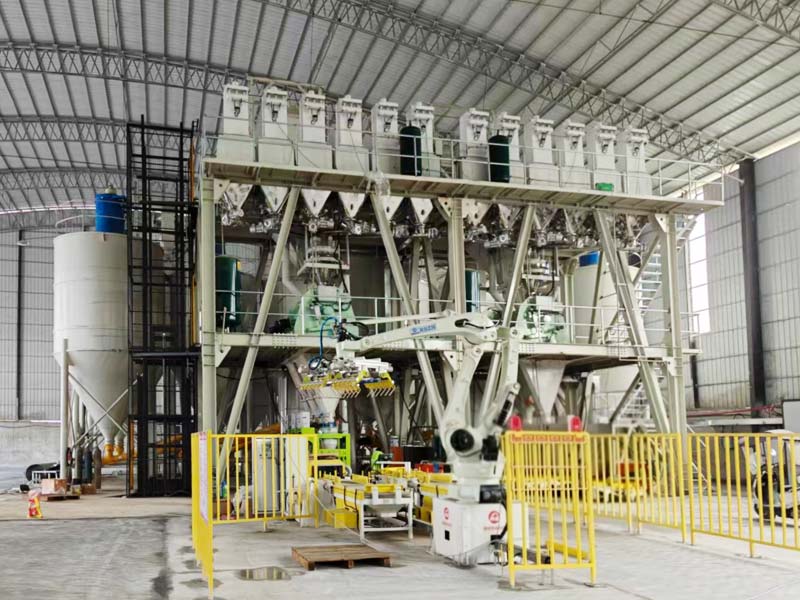
Prepare a controlled list of additive identities, intended batch sizes and the smallest and largest required quantities. Tile adhesive additive dosing becomes easier to assess when the supplier sees actual recipe quantities instead of a single statement that the line needs “high accuracy.” Include any trial products or small commercial batches that are part of the operating plan.
Record the physical information relevant to handling, such as supplier documentation, packaging, bulk density and known flow behavior. Two materials with similar names or dosing quantities may behave differently in a feeder. Ask the additive provider which characteristics need to be considered and obtain representative samples for agreed equipment trials.
Distinguish routine doses from exceptional development work. A system designed for regular commercial batches may need a different approved method for a much smaller pilot addition. Make that distinction explicit so a rare requirement does not silently become an unsupported operating condition during production.
Separate scale performance from feeder performance
A scale measures mass, while the feeding mechanism determines how material arrives and stops. Tile adhesive additive dosing needs a review of both. A fine display resolution does not establish that a powder feeder can stop consistently at the smallest recipe quantity or that material flow remains stable between refill conditions.
Ask how the measuring system is verified over the intended operating range. Request traceable results with test conditions, rather than a statement that the scale passed. Then review dynamic dosing trials with the actual or agreed representative material. Static verification and dynamic feeding answer related but different questions.
Discuss coarse and fine feeding, stopping behavior and the role of any adaptive control. The equipment supplier should explain how those features work within the proposed range. Avoid assuming that one percentage accuracy claim applies equally to a large dose and the smallest addition. The acceptance definition should identify the quantity and basis to which a tolerance applies.
Follow the material after weighing
The recorded weight is not the end of the process. Trace the additive through the weigh hopper, discharge valve, chute and mixer entry. Tile adhesive additive dosing can appear accurate at the scale while retained powder changes what actually reaches the mixer. Small doses make the material-transfer question particularly important.
Review the geometry and operating method of the transfer route with the supplier. Identify where powder can remain and how normal discharge is confirmed. Do not prescribe an improvised clearing method. The equipment instructions and material characteristics should determine the approved procedure, including any cleaning and access requirements.
Include transfer in the trial. Record the commanded quantity, measured quantity, discharge condition and relevant observations. If the system uses containers or manual additions for some materials, define how those containers are identified, checked and reconciled with the batch record. A separate handling step should remain traceable to the same production event.
Make material identity part of dosing control
Correct mass of the wrong material is still an incorrect addition. Define how incoming additives, storage positions and feed connections are identified. Tile adhesive additive dosing should include a procedure for refilling and confirming the correct material, especially where several similar bags or containers are handled in the same area.
Use the plant's controlled product and material codes rather than relying only on color or an informal nickname. Agree who verifies a refill and how the event is recorded. The method should fit the factory's workflow and remain practical during a busy shift. A complicated control that is routinely bypassed provides weak protection.
Review changes in additive grade or supplier through the formulation and quality process. A substitute may affect both product behavior and equipment handling. Do not treat a familiar material name as proof that the new grade can use the same feed settings. Retain the relevant approval and update the controlled records where required.
Compare dosing arrangements on the same basis
| Arrangement | Questions for the supplier | Bukti untuk diminta |
|---|---|---|
| Automatic small-additive feeder | What dose and material range is supported? | Repeated dosing results under defined conditions |
| Shared weigh hopper | How are ingredients separated and sequenced? | Recipe logic, transfer observations and cleaning review |
| Dedicated additive route | How does it connect to the mixer and batch record? | Interface drawing and verified material path |
| Controlled manual addition | How are identity, quantity and completion confirmed? | Approved procedure and traceable batch entry |
| Container-based preparation | What can remain in the container after transfer? | Handling trial and reconciliation method |
There is no universal best arrangement for every factory. Tile adhesive additive dosing should be evaluated against product range, batch frequency, staffing, handling properties and the consequences of a wrong addition. A buyer can compare offers fairly by providing the same dose table and requiring suppliers to identify the operating limits of their proposals.
Plan the refill condition into the trial
Feeding behavior can change as material level changes. Review the intended refill procedure and the conditions immediately before and after replenishment. A trial using one conveniently filled hopper may not represent a full production shift. Ask the supplier which material-level conditions should be included in verification.
Keep the powder condition representative. Packaging, storage and handling should follow the material provider's instructions. Tile adhesive additive dosing trials should record any condition that could affect flow, including an unusual lot or a handling change. The purpose is to understand normal operating behavior and credible variation, not to make one demonstration appear consistent.
Define what the operator should do when feeding is unstable or a dose cannot be completed normally. The process needs an agreed hold, review and recovery procedure. Do not allow repeated manual overrides to disappear from the record or turn an uncertain addition into an ordinary accepted batch without the required decision.
Verify the smallest dose repeatedly
Choose the trial quantities from the intended recipe range, including the smallest regular dose. Agree the number of repetitions, measurement method and acceptance criteria with the supplier and quality team. Retain individual results rather than recording only a rounded average. Tile adhesive additive dosing should demonstrate consistent behavior, not just a favorable mean.
Include representative operating conditions such as the agreed hopper levels and refill sequence. Record equipment settings and material identity so results can be reproduced. If an adjustment is made during testing, separate the before and after results rather than combining them into one apparently stable data set.
Investigate unsuccessful results. Check measurement, feeding and transfer separately before selecting a correction. A trial that reveals a lower practical dose limit is valuable procurement evidence. The buyer can then change the feeder arrangement, batch policy or approved handling method before the equipment is accepted.
Connect dosing with finished-product verification
The quality team should define which product tests are needed to confirm the intended tile-adhesive performance. Dosing data are part of the evidence, but they do not replace formulation validation or finished-product assessment. A correct recorded addition does not establish that mixing, packaging and storage preserved the intended result.
Link samples to batch identifiers and recipe versions. Tile adhesive additive dosing investigations become more useful when the team can compare a product result with its material lot, dosing record and production conditions. Avoid comparing unlinked laboratory samples with daily averages from the controller.
If product variation appears despite consistent dosing records, review the rest of the route. Potential investigation areas include raw-material variation, blending, discharge, segregation and sampling. The dosing system should remain part of a complete process review rather than being assumed responsible for every quality difference.
Turn the findings into a purchase specification
Include the additive list, minimum and maximum quantities, batch range, material documentation, required identification method and trial conditions in the technical brief. Ask the supplier to state any exclusions clearly. Tile adhesive additive dosing should have a defined acceptance scope that covers both the measuring system and material arrival at the mixer.
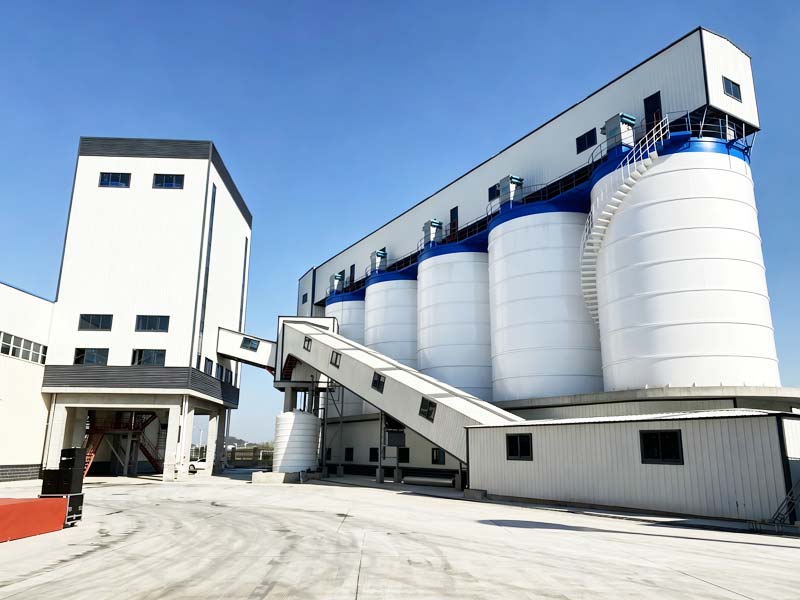
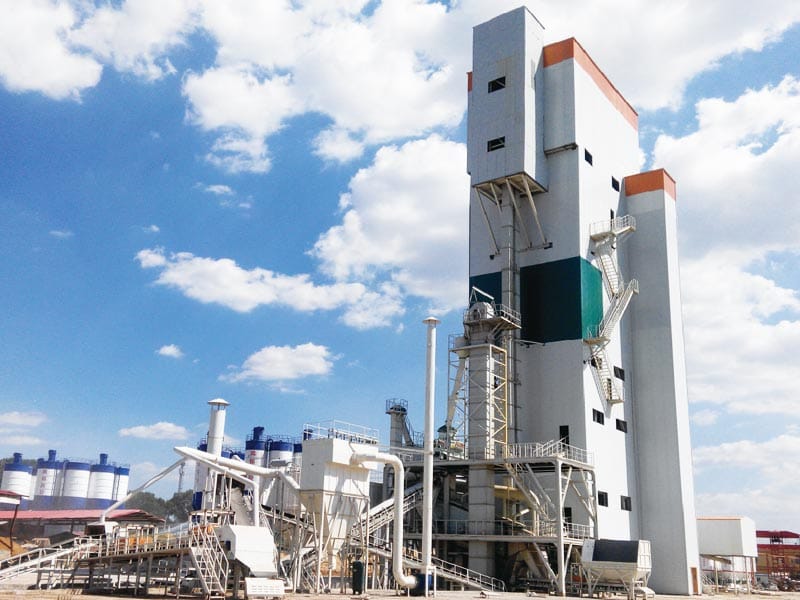
Discuss the requirements when reviewing Yunguan's pabrik pencampuran mortar kering tipe menara or tanaman mortar kering tipe langkah. Include future products only where their material and dose requirements can be described. A general request for unlimited formulation flexibility cannot be verified meaningfully.
The American Cement Association applications overview provides context for the range of cementitious materials and their differing composition. It does not prescribe tile-adhesive additive doses or verify a particular dosing system. Use the actual formulation and agreed equipment tests for those decisions.
Send your additive dose table, intended batch range and product list through the form below. Request a review of the smallest commercial dose, material identity controls, transfer route and acceptance-trial evidence.
Pertanyaan yang sering diajukan
Should tile adhesive additive dosing be selected only from the maximum quantity?
Review the complete range, including the smallest regular addition. Tile adhesive additive dosing can be limited by low-dose feeding and transfer even when the system can handle the maximum quantity.
Is scale calibration enough to accept the system?
No. Static measuring-system verification should be complemented by representative feeding and transfer trials. The combined system must deliver the intended material to the mixer.
Can manual additions be part of a controlled process?
They can be considered where the approved procedure defines identity, quantity, completion and traceable records. Suitability depends on the actual product, workflow and quality requirements.
Why should refill conditions be tested?
Material level and replenishment can affect feeding behavior. Tile adhesive additive dosing should be evaluated under representative conditions instead of only with one conveniently prepared hopper.
What if a new additive supplier is introduced?
Review the change through formulation and quality control, including relevant handling characteristics. Confirm whether equipment settings or validation need to change before routine production uses the new material.