Índice
Small batch concrete mixing exposes limitations that may be hidden when a plant runs its usual production volume. The mixer must work at the proposed fill level, scales must measure the smaller ingredient quantities, and the discharge route must deliver the batch without excessive retention. A successful full-load demonstration does not automatically validate a small architectural, repair or precast batch.
Begin with the smallest batch the factory expects to make routinely. Identify its recipe, destination, consistency and quality requirements. Then review the whole route from weighing to casting. This makes the equipment discussion more useful than asking whether a large mixer “can also make small quantities.” The answer depends on the actual operating range and how the surrounding systems handle it.
Define small batch concrete mixing quantities
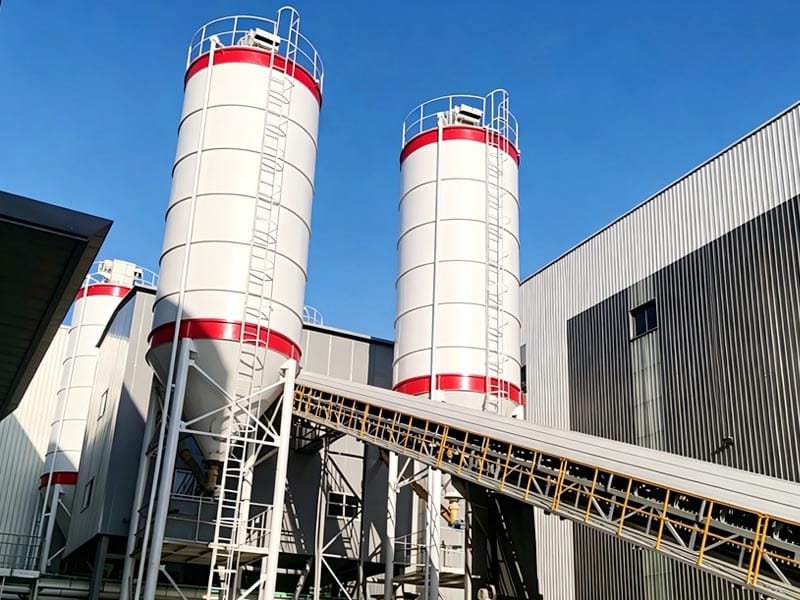
State the required finished batch volume and the corresponding ingredient quantities from the approved mixture design. The supplier needs both. Small batch concrete mixing should not be described solely as a fraction of mixer nameplate capacity because different products and consistency requirements can create different operating conditions.
Identify whether the small quantity is a routine commercial product, a color change, a laboratory-scale development batch or an occasional production adjustment. A plant designed around frequent small batches may need a different arrangement from one that produces them rarely. Record the expected frequency and the value of the product to help evaluate the cost of a dedicated solution.
Ask the mixer supplier to confirm the minimum recommended operating range for the proposed material and configuration. Keep that confirmation with the technical offer. Do not infer a universal minimum fill percentage from another mixer type or a general industry example. The relevant evidence is performance with the proposed equipment and product conditions.
Check every ingredient at its minimum dose
List the smallest cement, aggregate, water, pigment and admixture quantities that the plant must handle. A weighing system that is suitable for the maximum production batch may need separate consideration at the lower end. Small batch concrete mixing can make a small absolute feeding variation significant relative to the intended dose.
Ask how scales and dispensers are verified over the actual operating range. Distinguish the scale's indicated resolution from the combined performance of the feeding, stopping and material-transfer system. A fine digital display does not prove that a feeder can stop consistently at a very small quantity or that all measured material reaches the mixer.
Review where small ingredients are introduced. Long chutes, large containers and transfer devices can retain a meaningful portion of a small addition. Consider the material path and the supplier's approved handling method. The objective is a repeatable dose arriving at the intended stage, rather than a correct number on the controller followed by uncertain transfer.
Review the mixing action at low loading
The mixer must produce the required result within its approved operating range. Small batch concrete mixing may change how material engages with the mixing tools and how reliably the batch circulates. The equipment supplier should explain which batch sizes are supported and what trial evidence is available for the intended concrete.
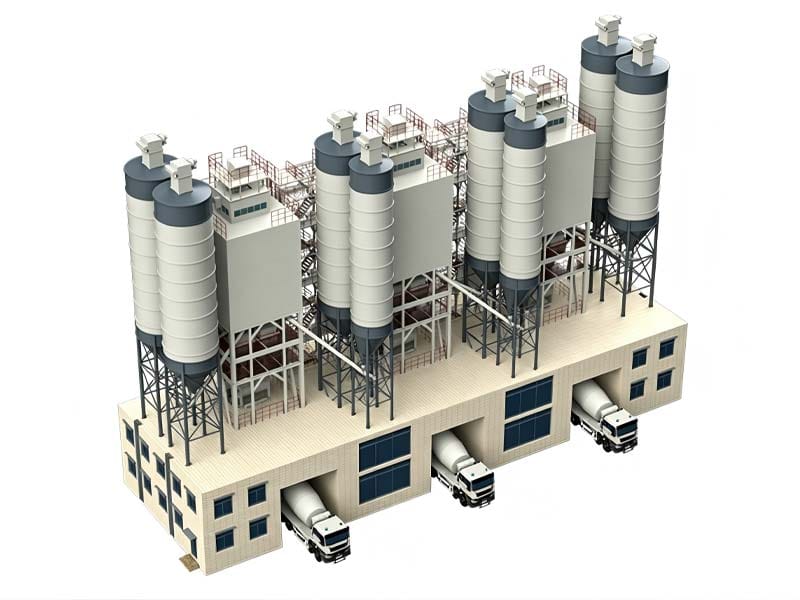
Compare the proposed mixer types using the actual product and line constraints. Yunguan's central dosadora de concreto pré-moldado is a relevant starting point for a precast discussion, but the complete configuration still needs review. Nominal mixer volume alone does not settle color distribution, consistency, discharge or the minimum effective batch.
Do not shorten or extend the mixing interval without an agreed trial. The quality team should define the measurements relevant to the product. A visually consistent batch may still need further evaluation, while a longer cycle can reduce the capacity available for frequent short runs. Keep product performance and production planning in the same discussion.
Measure the material that reaches the destination
Follow the batch through the discharge hopper, bucket, conveyor or other distribution equipment. Small batch concrete mixing only creates commercial value if the intended quantity reaches the casting operation in suitable condition. Retained material that is insignificant during a large run can represent an important part of a small batch.
Record the route and hold time during the trial. A test that discharges directly into a nearby container may not represent the factory's normal transport system. If the production line has several destinations, review the most demanding relevant route. Differences in transfer distance, waiting and discharge geometry can affect practical suitability.
Discuss how the receiving equipment recognizes and handles a small batch. The destination may have a minimum useful load or a cycle designed around larger deliveries. A plant can pass its own trial while the casting line struggles to use the material efficiently. Include the downstream equipment owner in the review so that the interface is tested rather than assumed.
Plan color and product changes
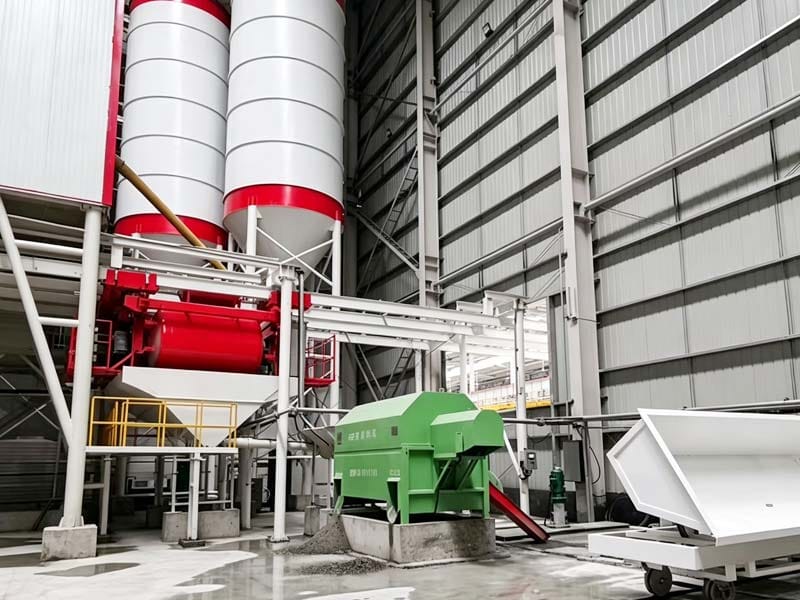
Small batches are often associated with specialty products, colors or short production runs. Define how the line changes between them. Small batch concrete mixing should include a review of cleaning, retained material and the disposition of transition production according to the factory's quality procedure.
Identify surfaces and transfer points shared between products. A mixer-only cleaning procedure may leave material in the discharge system or transport equipment. Ask what can be inspected and cleaned safely, how long the change takes and which activities require a shutdown. The production plan should reflect the complete line rather than a brochure claim about mixer cleaning.
Record cleaning and changeover conditions during the trial. If the first small batch after a change behaves differently from subsequent batches, investigate that pattern explicitly. Do not average the transition batch into a larger data set and lose the information needed to establish an operating procedure.
Compare three practical arrangements
| Arrangement | Potential fit | Questions to resolve |
|---|---|---|
| Existing main mixer within an approved small-batch range | Occasional short runs using compatible products | Minimum loading, low-dose accuracy and retained material |
| Separate smaller production mixer | Frequent small batches or a distinct specialty product | Shared weighing, distribution, cleaning and additional space |
| Dedicated development or pilot arrangement | Formulation work and limited trials | How results transfer to commercial production equipment |
The comparison should use the factory's real demand. A dedicated small system adds equipment and maintenance, while using the main line can consume valuable production time. Small batch concrete mixing decisions should account for total changeover and delivery time as well as the quantity produced in the mixer.
Avoid treating a pilot batch as automatic proof of full-scale performance. The formulation team should evaluate what changes when the recipe moves to another mixer, feeding arrangement or batch size. Equally, do not assume that a successful large batch validates the smallest commercial quantity. Each required operating region needs appropriate evidence.
Build a representative acceptance trial
Agree the recipes, minimum and normal batch sizes, raw materials, sampling points and quality criteria before testing. Include repeated small batches and a relevant changeover where those conditions are part of normal business. Record the actual ingredient measurements, cycle times, discharge behavior and destination information.
Small batch concrete mixing should be evaluated using product-relevant tests defined by the quality team. Where consistency or distribution is a concern, use a sampling plan capable of detecting meaningful variation. Do not rely solely on one convenient sample or a supplier's visual judgment during a demonstration.
Retain failed or unusual results and their associated production records. A trial is useful when it reveals the operating limit, not only when it produces an attractive demonstration. If a proposed small quantity cannot be made reliably, the buyer can change the configuration or commercial batch policy before routine production begins.
Calculate the production cost of a short run
Separate ingredient cost from line time, cleaning, transition material, testing and transport. Small batch concrete mixing can have a different cost structure from continuous production even when the recipe cost per cubic metre is similar. A comparison should show the cost of an actual order rather than multiplying the large-run unit cost by a smaller volume.
Use measured cycle and changeover times where possible. Record the period for which the main line is unavailable for other production. If a small specialty order interrupts a busy precast schedule, that lost production opportunity may matter to the equipment decision. Present it as a site-specific business calculation, without assuming that every factory has the same constraint.
Ask suppliers to separate the scope needed for minimum-load performance from optional automation or distribution features. This helps compare offers on a common basis. A lower initial price can be misleading if the quotation leaves the small-ingredient system or required downstream modification outside the package.
Prepare the specification for an equipment review
Provide a table of intended products, minimum and normal batch sizes, frequency, ingredients with small doses, destination routes and changeover requirements. Include the existing layout if this is an upgrade. Small batch concrete mixing becomes a concrete engineering discussion when the supplier can see the lower operating limit that the factory actually needs.
Review Yunguan's soluções pré-moldadas de concreto alongside the intended casting line and material route. Request confirmation of the proposed batch range, measuring-system suitability and acceptance-trial scope. The final specification should connect equipment capability with the product and production conditions under which it will be demonstrated.
O NRMCA production-facility certification overview emphasizes verification of measuring equipment within its program. It provides background for asking for traceable checks, but it does not establish the minimum batch size of a particular mixer or certify a proposed Yunguan configuration.
Send your smallest recipe, expected weekly demand and casting route through the form below. Ask for a configuration review that covers low-dose measurement, mixing, discharge and the cost of changing between products.
Frequently asked questions
Can small batch concrete mixing be qualified from vessel size alone?
The supplier should confirm its permitted operating range for the proposed concrete. Small batch concrete mixing depends on mixer loading, feeding, measurement and discharge, not only on available vessel space.
Does a precise scale display prove small-dose accuracy?
No. Review the complete measuring and feeding system at the intended quantity, including stopping behavior and transfer to the mixer. Display resolution is only one aspect of the system.
Why can discharge retention matter more for a small batch?
A retained quantity represents a larger share of a small batch. Review what reaches the destination and how shared discharge equipment affects product changes and usable yield.
When is a separate small mixer worth considering?
Consider it when frequent short runs, specialty products or changeovers constrain the main line. Compare equipment cost with the actual production time, cleaning and destination requirements of those orders.
What should an acceptance trial demonstrate?
It should demonstrate the agreed minimum and normal batch conditions through the real material route, with repeat measurements and product-relevant quality checks. Include a representative changeover where required.