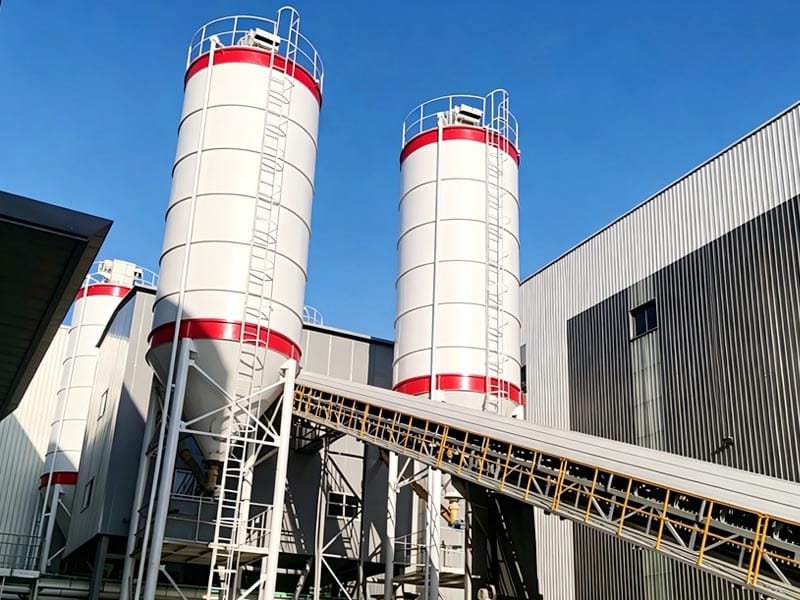
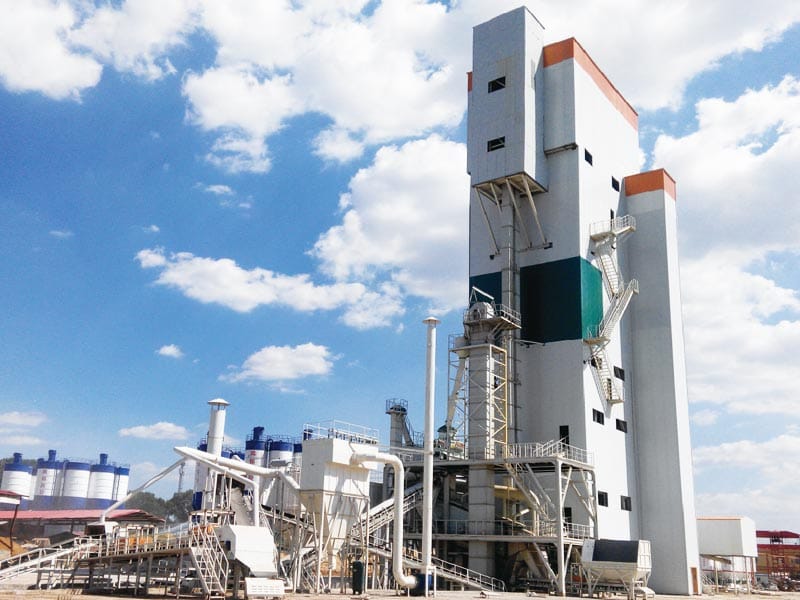
Masonry mortar production is a complete manufacturing process that starts with raw-material control and ends with finished mortar being packed, stored or dispatched in bulk. The production line has to manage sand grading, cementitious materials, additives, weighing, dry mixing, finished-product buffering and delivery without allowing moisture, segregation or cross-contamination to change the product.
For equipment buyers, the important question is not simply how many tonnes per hour a dry mortar plant can produce. The plant should be configured around the actual masonry mortar types, sand specification, recipe range, packaging method and dispatch model.
Nostro impianto di miscelazione di malta secca del tipo a torre is designed for large-scale dry mortar production and explicitly includes masonry mortar among its applications. This guide explains how masonry mortar production should be planned from aggregate intake through final dispatch.
What Is Masonry Mortar Production?
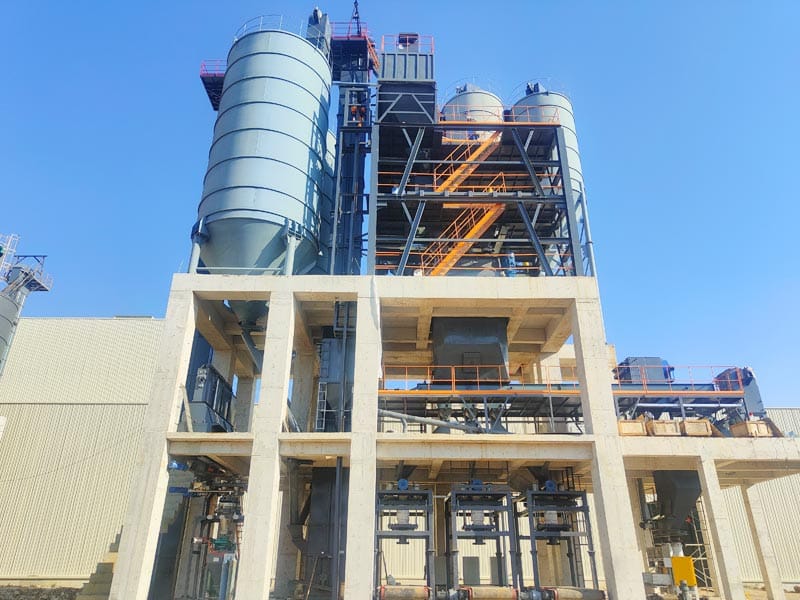
Masonry mortar production is the controlled manufacture of dry mortar intended for laying masonry units such as bricks, blocks or other unit masonry products.
The dry factory process can include:
- sand receiving;
- sand drying or use of pre-dried sand;
- screening and classification;
- sand storage;
- cementitious-material storage;
- additive storage;
- pesatura;
- dry mixing;
- finished-product storage;
- bagging or bulk dispatch.
The final mortar is normally mixed with water at the point of use according to the product instructions and applicable specification.
Start with the Governing Mortar Specification
ASTM C270-26 currently covers mortar for unit masonry and includes both proportion and property specifications.
For masonry mortar production, that distinction matters because the factory should know whether the product is being controlled by:
- a defined material proportion;
- specified laboratory properties;
- another regional product standard;
- a customer-specific approved formulation.
The production line should reproduce the approved formulation consistently rather than invent its own mortar type from equipment settings.
Do Not Use Field Mortar Strength as the Factory Acceptance Shortcut
ASTM C270-26 specifically notes that field-sampled mortar strength should not be used to determine compliance with the standard in the same way as laboratory-qualified mortar.
For masonry mortar production, the plant should instead maintain control over:
- approved raw materials;
- correct proportions;
- registrazioni batch;
- mixing procedure;
- test del prodotto finito.
Sand Is Usually the Largest Material Stream
In most masonry mortar production lines, sand represents the largest mass flow.
That makes sand handling a major factor in:
- plant capacity;
- storage volume;
- drying energy;
- tempo di pesatura;
- finished mortar consistency.
The sand system should therefore be specified before selecting silo and mixer sizes.
Use the Correct Aggregate Standard
ASTM C144-26 covers aggregate for masonry mortar and recognizes both natural sand and manufactured sand.
The standard requires suitable grading and controls deleterious substances for the intended masonry mortar use.
For masonry mortar production, provide:
- fonte di sabbia;
- grading curve;
- dimensione massima delle particelle;
- densità apparente;
- umidità;
- deleterious-material test results where required.
Nostro guida curva di classificazione della sabbia explains why the full sieve distribution is more useful than one nominal size.
Manufactured Sand Can Be Used for Masonry Mortar
ASTM C144-26 explicitly recognizes manufactured sand as a possible masonry mortar aggregate when it is specially processed to achieve suitable grading.
This is important for integrated plants because manufactured sand can be produced and classified for downstream mortar use.
However, masonry mortar production should not accept manufactured sand only because it is below a certain maximum size.
Controllo:
- grading;
- contenuto di polvere;
- clay-related quality;
- forma delle particelle;
- product performance.
Sand Moisture Must Be Controlled Before Dry Mixing
Dry mortar production requires sufficiently dry aggregate.
Wet sand can cause:
- agglomerazione; agglomerazione;
- poor powder flow;
- pesatura instabile;
- premature reactions;
- packaging problems.
Masonry mortar production should therefore control sand moisture before the material reaches long-term dry storage.
Dry Sand Storage Should Preserve Grading and Flow
After drying and classification, sand still needs to remain:
- dry;
- free-flowing;
- separated by fraction;
- protected from contamination.
Nostro dry mortar sand storage guide explains how bridging, ratholing, segregation and usable capacity can affect production.
Do Not Size Every Sand Bin Equally
One sand fraction may be used in almost every masonry mortar recipe, while another may only be used in selected products.
Storage should therefore follow actual consumption.
| Storage question | Perché è importante |
|---|---|
| Which fraction is used most? | Defines the largest routine buffer |
| How often is sand replenished? | Defines required autonomy |
| What is the bulk density? | Converts tonnes to storage volume |
| How many mortar recipes share the fraction? | Defines consumption variability |
Cementitious Materials Need Dedicated Storage and Identification
Masonry mortar production can use cement, lime or other approved cementitious materials depending on the product specification.
Each bulk powder should have:
- dedicated storage identification;
- controlled tanker connection;
- reliable silo discharge;
- independent weighing;
- batch traceability.
The correct mass of the wrong cementitious material is still an incorrect batch.
Bulk Powder Flow Can Limit Production
Fine cementitious powders can:
- bridge;
- rathole;
- aerate;
- compact;
- feed inconsistently.
For masonry mortar production, powder storage and screw feeding should be designed around real material behavior rather than only maximum screw throughput.
Additives Need Their Own Dosing Strategy
Masonry mortar formulations can include functional additives depending on the target product.
These may be used at much smaller quantities than sand or cement.
For masonry mortar production, define:
- additive name;
- dose minima;
- dose massima;
- densità apparente;
- scorrevolezza;
- manual or automatic dosing method.
Nostro mortar additive dosing guide explains why low-dose ingredients often need separate equipment.
Micro-Dosing Should Be Validated at the Smallest Target
A dosing system that performs well at 20 kg may not perform equally well at 1 kg.
For low-dose materials, masonry mortar production should verify:
- scale resolution;
- feeder cutoff;
- material in flight;
- ripetibilità;
- final batch records.
Recipe Management Should Control Material Identity and Quantity
A modern dry mortar plant should store approved recipes in the control system.
The recipe can define:
- frazioni di sabbia;
- materiali cementizi;
- riempitivi;
- additives;
- dimensione del lotto;
- sequenza miscelazione.
Masonry mortar production should use controlled recipe revisions so operators do not make undocumented changes during routine production.
Separate Weighing Systems Improve Process Control
Sand, bulk powder and micro-additives operate at very different mass ranges.
Using dedicated scales allows each group to be matched to a more appropriate capacity and resolution.
For masonry mortar production, review:
- sand scale;
- powder scale;
- micro-additive scale;
- minimum and maximum targets;
- mechanical isolation.
Weighing Accuracy and Dosing Control Are Different
A scale can be correctly calibrated while the feeder still overshoots.
Causes can include:
- screw coast-down;
- material in flight;
- coarse feed stopping too late;
- unstable powder flow.
Nostro dry mortar dosing overshoot guide explains how batch records can distinguish measuring problems from feeder problems.
Mixing Sequence Should Follow the Product
Not every masonry mortar recipe needs the same charging sequence.
A practical sequence can include:
- major sand and powder charging;
- filler addition;
- micro-additive addition;
- omogeneizzazione finale.
The exact sequence should be validated using the actual formulation.
Mixing Time Should Be Established by Uniformity
There is no universal dry mixing time for all masonry mortar production.
The required duration depends on:
- progettazione del miscelatore;
- livello di riempimento del lotto;
- ingredient count;
- classificazione della sabbia;
- additive dose;
- sequenza miscelazione.
Use finished-product uniformity and performance to establish the production setting.
Overmixing Can Reduce Line Output
Once the batch has reached the required homogeneity, extra mixing time can reduce hourly output without improving the product.
Commissioning should therefore compare:
- durata della miscelazione;
- uniformity;
- finished mortar test results;
- cycle time.
Batch Size Should Match the Mixer Working Range
A dry mortar mixer performs best within its intended operating range.
For masonry mortar production, validate:
- lotto normale;
- lotto minimo di routine;
- lotto massimo;
- complete discharge.
Do not assume a small specialty batch will mix identically to a full ordinary-mortar batch.
Tower-Type Plants Suit Large Repetitive Mortar Production
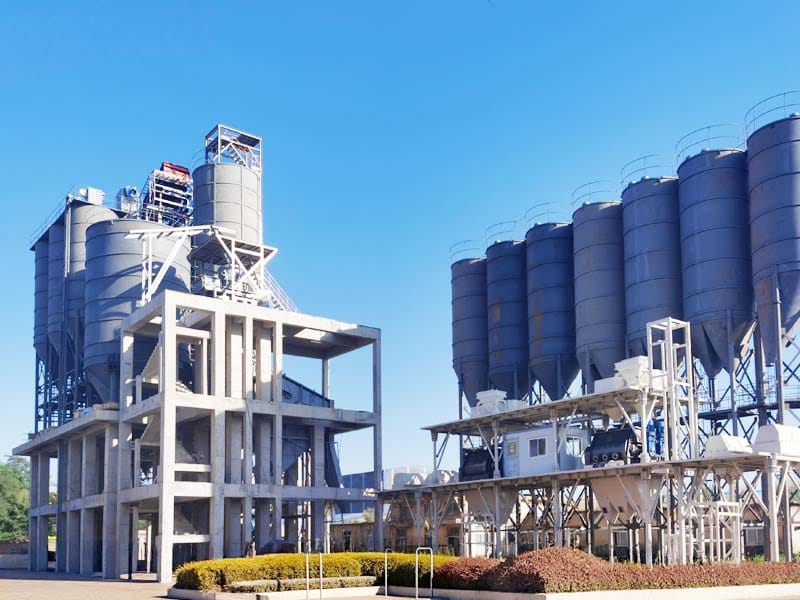
The current MixingPlantPro tower-type plant uses a vertically integrated process where raw materials enter upper storage and move by gravity through batching, mixing, finished-product storage and packaging.
The product page explicitly lists masonry mortar among the supported product types.
For masonry mortar production, this layout can be useful where:
- production is continuous;
- large raw-material storage is required;
- the site favors vertical integration;
- automated bag and bulk dispatch are important.
Public capacity figures should still be confirmed against the final project specification and product mix.
Step-Type Plants Can Balance Height and Process Integration
Step-type dry mortar plants combine vertical staging with horizontal transfer between levels.
For masonry mortar production, this can offer a different balance between:
- altezza dell'edificio;
- equipment access;
- trasferimento materiale;
- storage arrangement.
Because public step-type capacity fields have shown inconsistency across website versions, the final capacity should come from the project proposal rather than a generic webpage number.
Workshop-Type Plants Can Support Flexible Product Changes
Workshop-type plants place the core equipment on a more horizontal factory-floor arrangement.
This can be useful when masonry mortar production shares equipment with:
- plaster mortar;
- repair mortar;
- tile adhesive;
- altri prodotti speciali.
More frequent changeovers increase the importance of cleaning access and recipe control.
Product Changeover Should Be Planned in Advance
If the same plant produces several dry mortar types, residual material from the previous product can enter the next batch.
Ispezionare:
- pesare tramogge;
- trasportatori a vite;
- miscelatore;
- finished-product buffer;
- packaging feeder.
Nostro guida di pulizia del miscelatore di malta secca explains how changeover requirements can be classified by product risk.
Water Should Stay Out of the Dry Process
Masonry mortar production is a dry manufacturing process.
Uncontrolled water can cause:
- agglomerazione; agglomerazione;
- hardened residue;
- corrosion;
- poor powder flow;
- storage problems.
Wet cleaning should only be used where the equipment procedure explicitly allows it and complete drying can be verified.
Finished-Product Buffering Separates Mixing from Packaging
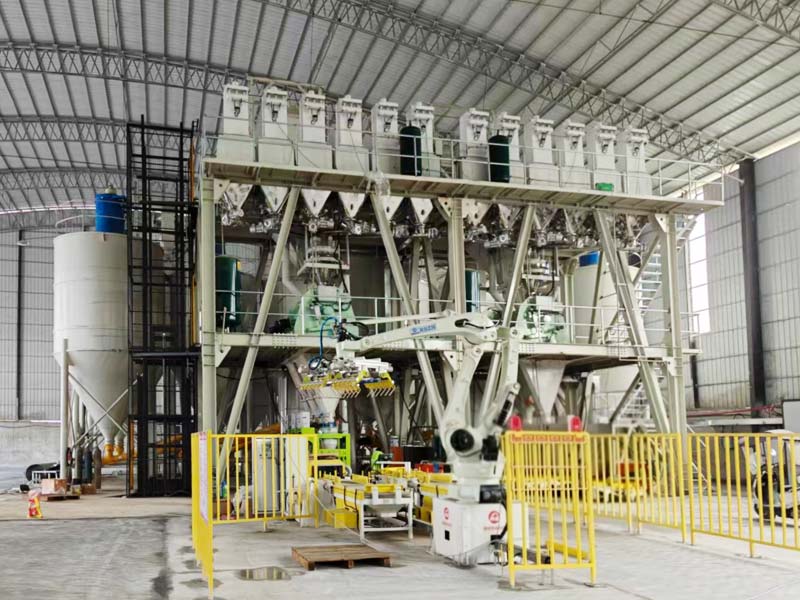
A finished-mortar hopper can allow the mixer to discharge and begin the next batch while packaging equipment handles the previous batch.
This can improve line utilization.
For masonry mortar production, review:
- buffer capacity;
- residence time;
- scorrevolezza;
- segregation risk;
- cleanout access.
Buffer Hopper Flow Can Become a Hidden Bottleneck
A mixer may finish batches faster than the buffer hopper can discharge to the packer.
If finished mortar bridges or ratholes, upstream production eventually stops.
Buffer design should therefore be checked using the actual finished mortar, not only raw sand flow data.
Bagging and Bulk Dispatch Need Different Downstream Equipment
Masonry mortar production can be dispatched as:
- bagged product;
- bulk product;
- both.
The production line should define how each route is isolated and controlled.
| Dispatch mode | Main equipment questions |
|---|---|
| Bagging | Bag size, filling rate, dust, weight control |
| Bulk | Finished silo, loading point, tanker interface |
| Combined | Routing, buffer capacity, production scheduling |
Bag Weight Control Depends on Product Flow
An accurate packer still needs stable material flow from the upstream hopper.
Changes in:
- densità apparente;
- aerazione;
- livello della tramoggia;
- agglomerazione; agglomerazione;
- ponte;
can change filling behavior.
Nostro guida alla variazione del peso del sacco di malta explains how packaging errors can originate upstream of the scale.
Bag Packaging Should Protect the Dry Product
After production, the package becomes a major moisture barrier.
For masonry mortar production, validate:
- bag material;
- valve or closure;
- finished-product temperature;
- integrità della borsa;
- warehouse storage.
Bulk Loading Needs Dust and Routing Control
If finished mortar is dispatched in bulk, the loading system should provide:
- correct silo selection;
- controlled loading rate;
- raccolta polveri;
- tanker identification;
- batch or lot traceability.
The bulk route should not allow accidental mixing between different mortar products.
Finished Product Storage Should Follow FIFO Logic
Long residence time can increase caking or inventory-control risk.
Where practical, finished mortar should follow a first-in/first-out operating strategy.
Masonry mortar production records should connect storage or packaging lots with the original production batches.
Dust Control Is Needed Across the Whole Line
La polvere può essere generata durante:
- sand transfer;
- powder silo filling;
- pesatura;
- carica del miscelatore;
- scarico del miscelatore;
- imballaggio;
- bulk loading.
The MixingPlantPro tower-type line uses enclosed negative-pressure operation and pulse dust collection in its current published configuration.
Dust collection should be maintained as part of normal masonry mortar production, not treated as separate auxiliary equipment.
Batch Records Should Support Product Traceability
A useful batch record can include:
- ID lotto;
- recipe revision;
- target quantities;
- actual quantities;
- tempo di miscelazione;
- allarmi;
- operatore;
- packaging or bulk lot.
This makes it easier to investigate product complaints or process drift.
Quality Control Should Link Raw Materials and Finished Tests
ASTM C270-26 verifies compliance through specified materials, proportions and applicable property testing rather than one field strength number.
For masonry mortar production, connect finished product results with:
- sand lot;
- cementitious-material lot;
- additive lot;
- batch record;
- packaging lot.
Commission the Plant with the Actual Masonry Mortar Formula
No-load factory testing cannot prove product performance.
Commissioning should verify:
- sand flow;
- flusso di polvere;
- microdosaggio;
- weighing repeatability;
- miscelazione;
- buffer discharge;
- bagging or bulk loading;
- batch records.
Finished mortar should then be tested according to the applicable product specification.
Run Consecutive Batches to Check Repeatability
One successful batch is not enough.
For masonry mortar production, compare several consecutive batches for:
- ingredient deviations;
- tempo di miscelazione;
- cycle time;
- finished density;
- packaging performance;
- finished-product test results.
What Should Buyers Send for a Masonry Mortar Line Review?
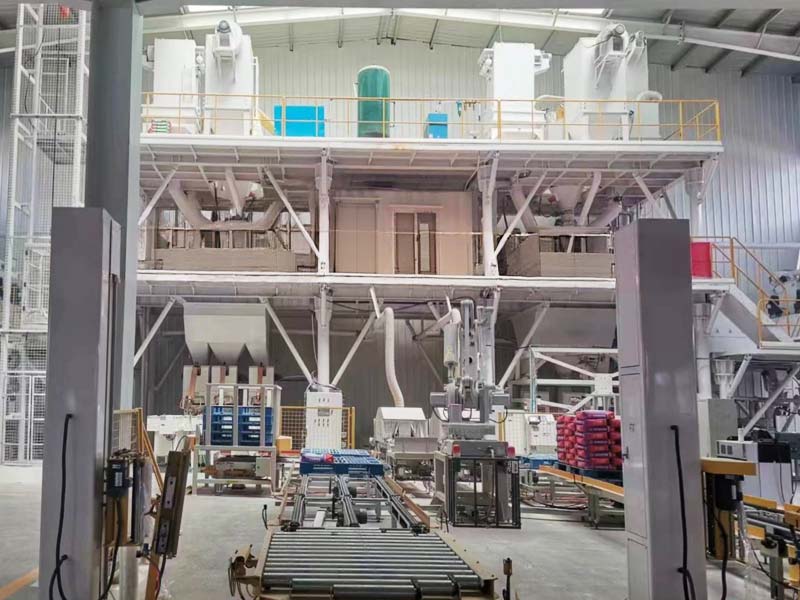
A useful masonry mortar production review needs the real product and dispatch requirements.
Fornire:
- mortar types;
- applicable specification;
- classificazione della sabbia;
- raw-material list;
- dose minima di additivo;
- dimensione normale del lotto;
- required finished output;
- dimensione della borsa;
- bulk dispatch requirement;
- frequenza di cambio prodotto;
- site dimensions.
Nostro soluzioni di malta secca can then be configured around the actual raw materials, product portfolio and dispatch model.
Send your mortar product requirements and raw-material information through our pagina contatti for a line review.
Conclusione
Masonry mortar production should be designed as a complete dry process from sand preparation and storage through weighing, mixing, finished-product buffering and dispatch.
The strongest plant specification starts with the governing mortar standard, sand grading, cementitious system, additive range and packaging method rather than one headline tonnes-per-hour target.
When raw-material handling, dosing, mixing and dispatch are engineered as one process, the plant can produce more consistent masonry mortar while reducing caking, cross-contamination, packaging variation and production bottlenecks.
FAQ
What equipment is needed for masonry mortar production?
A complete line can include sand preparation and storage, powder silos, additive storage, weighing, dry mixing, finished-product buffering, dust collection, bagging and bulk loading.
Can manufactured sand be used in masonry mortar?
Yes. ASTM C144-26 recognizes manufactured sand for masonry mortar when it is properly processed and meets the required grading and quality criteria.
What standard covers mortar for unit masonry?
ASTM C270-26 covers mortar for unit masonry and includes proportion and property specification approaches. Local or project-specific standards may also apply.
Why is additive dosing important in masonry mortar production?
Functional additives can be used at much lower quantities than sand or cement, so scale range, feeder behavior and repeatability can strongly affect formulation consistency.
What information should I provide before selecting a masonry mortar plant?
Provide mortar types, sand grading, raw materials, dose ranges, batch size, output requirement, packaging method, bulk-loading needs and site dimensions.