Skip hoist maintenance is essential for concrete batching plants that lift weighed aggregate vertically from the batching section to the mixer. Unlike a continuous belt conveyor, a skip hoist repeatedly accelerates, travels, decelerates, stops and returns through the same lifting path. That cycle puts repeated demand on the wire ropes, drum or drive system, guide components, brakes, limit switches and hopper structure.
For plant teams, the correct maintenance approach is not simply to inspect the bucket when something begins making noise. The entire lifting system should be treated as one mechanical and control chain, because a fault in a limit switch, rope, guide, brake or loading sequence can affect both production and safe operation.
لدينا مصنع خلط الخرسانة المثبت على الجانب و مصنع خلط الخرسانة بدلو علوي use intermittent vertical aggregate lifting with a double-wire-rope synchronous lifting system and multiple limit protections. This guide explains what a practical skip hoist maintenance inspection should cover.
Why Skip Hoist Maintenance Is Different from Belt Conveyor Maintenance
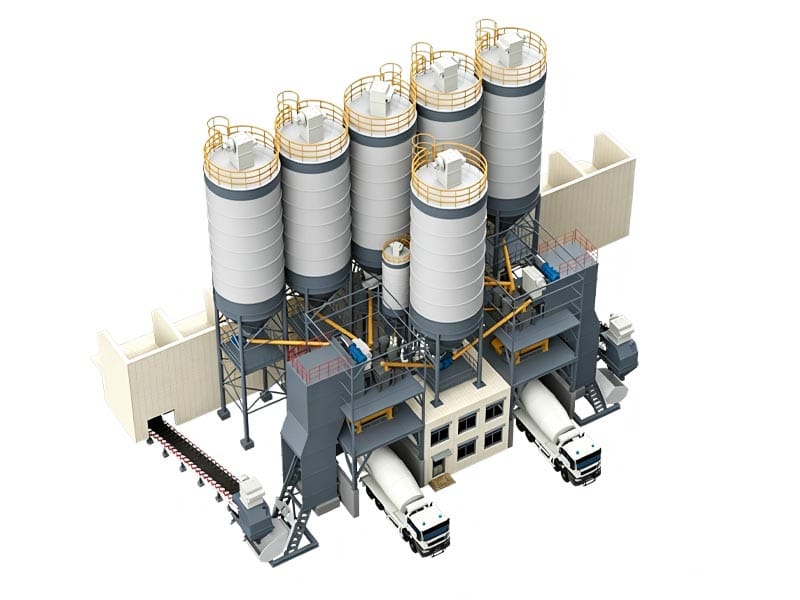
A belt conveyor moves aggregate continuously along a relatively fixed path.
A skip hoist operates as a repeated lifting cycle:
- the hopper receives weighed aggregate;
- the lifting drive starts;
- the hopper accelerates upward;
- it travels along the guide path;
- it decelerates near the top;
- it reaches the discharge position;
- aggregate is released;
- the hopper returns to the lower position.
Skip hoist maintenance therefore needs to consider both mechanical wear and movement control.
Start with a Repeatable Inspection Route
A routine inspection should cover the same components in the same order.
| Inspection area | ماذا تتحقق | Possible warning sign |
|---|---|---|
| Skip hopper | Body, liners, gate and fasteners | Cracks, deformation or material leakage |
| Wire ropes | Visible condition and equal behavior | Broken wires, distortion or unequal tension |
| Guide system | Alignment, wear and obstruction | Rubbing, impact or irregular travel |
| Drive system | Motor, gearbox, drum and coupling | Noise, heat, vibration or oil leakage |
| Braking system | Stopping and holding behavior | Drift, delayed stop or abnormal noise |
| Limit devices | Position detection and protection | Late stopping or inconsistent position |
Skip hoist maintenance becomes more useful when results are recorded rather than checked only by memory.
Inspect the Skip Hopper Structure
The skip itself experiences repeated loading and unloading.
يفتش:
- hopper body;
- welds;
- reinforcement areas;
- wear liners where fitted;
- mounting points;
- gate structure;
- rope attachment points.
Look for cracks, distortion, loose fasteners and areas where aggregate impact has worn the structure.
Skip hoist maintenance should address structural damage before it changes the hopper’s travel or load distribution.
Check the Hopper Gate and Discharge Mechanism
The skip must discharge aggregate completely at the top of the lifting path.
Residual aggregate can change the next cycle’s load.
يفحص:
- gate opening;
- gate closing;
- hinges or pivots;
- wear surfaces;
- تراكم المواد؛;
- position feedback where included.
If the hopper returns with material still inside, investigate the discharge mechanism before adjusting the batching sequence.
Wire Rope Condition Is a Core Inspection Item
MixingPlantPro’s current side-mounted and overhead bucket plants both specify a double-wire-rope synchronous lifting system.
For skip hoist maintenance, inspect each rope for visible changes such as:
- broken wires;
- kinks;
- flattening;
- corrosion;
- abrasion;
- diameter change;
- damage near terminations.
Wire-rope rejection criteria should follow the equipment manufacturer, rope supplier and applicable lifting standard. Do not invent a universal broken-wire count or diameter-loss limit for every skip hoist.
Compare the Two Ropes, Not Only Each Rope Individually
A dual-rope system depends on both ropes sharing the lifting duty correctly.
During skip hoist maintenance, compare:
- rope length;
- tension;
- wear pattern;
- drum winding;
- attachment condition.
If one rope consistently appears tighter or looser than the other, investigate the synchronization and attachment system.
The goal is not merely that both ropes remain intact. They should also operate together as designed.
Inspect Rope Terminations and Attachment Points
Wire ropes transfer load through their end connections.
يفحص:
- rope sockets or clamps;
- pins;
- shackles where fitted;
- retaining hardware;
- mounting plates;
- deformation around the attachment.
Skip hoist maintenance should treat the termination as part of the rope system rather than inspecting only the visible free length.
Check Rope Winding on the Drum
If the hoist uses a winding drum, the rope should spool in the intended pattern.
Look for:
- crossed wraps;
- overlapping rope;
- uneven winding;
- groove wear;
- rope rubbing against flanges.
Irregular winding can create localized rope damage and uneven lifting behavior.
Inspect the Drum Surface and Grooves
The drum should support the rope without sharp wear points.
During skip hoist maintenance, inspect:
- groove condition;
- surface wear;
- cracks;
- السحابات؛;
- rope anchorage;
- alignment with the lifting path.
If the rope repeatedly wears in the same location, inspect both the rope and the component it contacts.
Guide Rails Should Remain Aligned
The skip hopper travels along a defined guide path.
Misalignment can cause:
- rubbing;
- impact;
- uneven wheel or guide wear;
- higher drive load;
- poor stopping position.
For skip hoist maintenance, inspect the guide system from bottom to top.
Look for loose supports, bent sections, settlement and signs that the hopper contacts the structure during travel.
Guide Rollers or Wheels Need Condition Checks
Where the hopper uses guide rollers or wheels, inspect:
- free rotation;
- تحمل الضوضاء؛;
- flat spots;
- wear;
- mounting bolts;
- alignment.
A damaged guide roller can make the hopper travel roughly even when the lifting ropes and drive are in good condition.
Watch the Hoist Travel During Normal Operation
Some symptoms are easier to detect while the skip is moving.
From a safe guarded location, observe:
- smooth acceleration;
- stable upward travel;
- unexpected sway;
- impact against guides;
- smooth deceleration;
- repeatable top and bottom positions.
Skip hoist maintenance should use operational observation to decide where a shutdown inspection is needed.
Jerking or Sudden Movement Needs Investigation
A skip hopper should not repeatedly jerk or shock-load the lifting system.
Possible causes include:
- drive-control problems;
- mechanical obstruction;
- brake behavior;
- rope tension differences;
- guide misalignment;
- load imbalance.
Do not compensate for repeated jerking only by changing control parameters before mechanical conditions are checked.
Check the Hoist Motor and Gearbox
The drive system provides repeated lifting torque.
يفتش:
- motor temperature;
- motor current where monitored;
- gearbox oil level;
- oil leaks;
- ضجيج؛;
- اهتزاز؛;
- mounting bolts.
Trend changes over time rather than relying only on one spot reading.
Inspect Couplings and Drive Connections
Mechanical connections between motor, gearbox and drum should remain aligned and secure.
يفحص:
- coupling wear;
- guard condition;
- loose bolts;
- misalignment;
- abnormal vibration.
After major drive-component replacement, alignment should be verified according to the equipment procedure.
Braking Performance Should Be Repeatable
The brake is part of the skip’s motion-control system.
Operators should pay attention to:
- stopping distance;
- holding behavior;
- unexpected drift;
- ضجيج؛;
- heat;
- changes after adjustment.
Skip hoist maintenance should follow the manufacturer’s specified brake inspection and adjustment procedure.
Do not apply a generic brake-clearance value from another hoist.
Limit Switches Control the Travel Boundaries
MixingPlantPro’s current bucket-plant pages specify multiple limit protections.
Limit devices can identify positions such as:
- lower loading position;
- deceleration point;
- upper discharge position;
- overtravel protection.
The exact arrangement depends on the model and control design.
Skip hoist maintenance should verify that each device is secure, correctly positioned and gives repeatable feedback.
Do Not Defeat a Limit Switch to Keep Production Running
If a position switch repeatedly trips or fails to detect the hopper, bypassing it can remove an important protection layer.
Instead, inspect:
- sensor alignment;
- mounting;
- target position;
- cable;
- PLC input;
- mechanical travel.
The root cause may be mechanical rather than electrical.
Check the Bottom Loading Position
The hopper should stop consistently where aggregate is discharged into it.
If the bottom position changes, problems can include:
- aggregate spillage;
- off-center loading;
- impact damage;
- incomplete hopper filling.
For skip hoist maintenance, compare actual hopper position with the chute and loading geometry.
Check the Top Discharge Position
At the top of travel, the hopper must reach the intended discharge point without excessive impact.
يفتش:
- stopping repeatability;
- discharge alignment;
- gate operation;
- receiving hopper condition;
- material spillage.
A changing top position can indicate limit-device, brake, rope or drive issues.
Aggregate Spillage Can Reveal a Hoist Problem
Spillage around the skip path is not only a housekeeping issue.
It can indicate:
- overfilled hopper;
- off-center loading;
- hopper deformation;
- gate leakage;
- rough travel;
- incorrect stopping position.
Skip hoist maintenance should record where spillage appears and during which stage of the cycle.
Do Not Overload the Skip Hopper
The batching and control system should match aggregate batch mass with the designed skip capacity.
Overloading can increase stress on:
- wire ropes;
- drive system;
- brake;
- hopper structure;
- guide components.
The allowable load should follow the actual equipment design and manufacturer documentation.
Aggregate Distribution Inside the Hopper Matters
If the aggregate stream enters strongly to one side, the hopper load can become uneven.
For skip hoist maintenance, check:
- loading chute position;
- aggregate trajectory;
- bin discharge sequence;
- hopper centering.
Repeated uneven loading can contribute to asymmetric wear or unstable travel.
Clean Material from the Hoist Path
Spilled aggregate can accumulate near:
- guide rails;
- bottom stops;
- sensors;
- rope paths;
- structural members.
Material buildup can interfere with normal movement.
Cleaning should be carried out under the appropriate safe isolation procedure when workers can be exposed to unexpected movement.
Lubricate Only the Points Specified by the Manufacturer
Skip systems include bearings, gearbox components and possibly other lubricated points.
However, not every moving surface should be greased.
لدينا batching plant lubrication guide explains why lubricant type, quantity and interval should be component-specific.
For skip hoist maintenance, maintain a lubrication register covering:
- bearing points;
- gearbox oil;
- approved grease points;
- مواصفات مواد التشحيم؛;
- service interval.
Rope Lubrication Must Follow Rope and Hoist Requirements
Wire-rope lubrication requirements vary with rope construction, environment and equipment design.
Do not apply arbitrary grease or oil to a rope without confirming compatibility and manufacturer instructions.
An unsuitable lubricant can attract abrasive contamination or interfere with inspection.
Check Electrical Cables Along the Hoist System
Position sensors, motors and control devices depend on cables remaining protected.
يفتش:
- cable abrasion;
- loose conduit;
- damaged glands;
- water ingress;
- sensor connections.
Intermittent electrical faults can appear as irregular stopping or unexplained alarms.
Use Alarm History to Support Mechanical Inspection
The control system can help identify recurring skip problems.
Review alarms for:
- travel timeout;
- limit-switch fault;
- motor overload;
- position mismatch;
- emergency stop.
Skip hoist maintenance becomes more precise when mechanical observations are compared with the alarm timeline.
Trend Travel Time
A gradual increase in travel time can indicate developing resistance even before a complete failure occurs.
Possible causes include:
- guide friction;
- drive wear;
- brake drag;
- mechanical buildup;
- changed load.
Record travel time under similar load conditions to make the trend meaningful.
Trend Motor Current Where Available
Motor current can provide another condition indicator.
If the same loaded skip cycle begins requiring more current, inspect:
- mechanical drag;
- guide condition;
- rope system;
- علبة التروس؛;
- load level.
Current trend does not identify the cause alone, but it can help identify a developing problem.
Safety Inspection Is Part of Maintenance
Skip-hoist maintenance work can expose personnel to unexpected movement, stored energy and falling material.
OSHA’s general hazardous-energy control standard requires lockout/tagout where servicing exposes employees to unexpected energization, startup or release of stored energy.
For skip hoist maintenance, the plant procedure should address:
- electrical power;
- gravity movement;
- stored mechanical energy;
- pneumatic gates;
- upstream aggregate feed.
Do Not Work Under an Unsupported Skip
A raised hopper represents stored gravitational energy.
If maintenance requires access beneath or near a raised skip, the equipment should be secured using the manufacturer-approved mechanical support or blocking method in addition to the required energy isolation.
Control logic or a brake command alone should not be treated as a physical maintenance support.
Lockout/Tagout Applies Before Hazardous Servicing
OSHA 1910.147 covers servicing and maintenance where employees can be exposed to unexpected machine startup or stored energy.
Tasks that can require isolation include:
- rope inspection requiring close access;
- guide repair;
- idler or wheel replacement;
- brake adjustment;
- jam removal;
- hopper repair.
The exact energy-control procedure should be established for the installed plant.
Do Not Apply Personnel-Hoist Inspection Rules Directly to Aggregate Skips
Some regulations contain detailed inspection intervals for personnel hoists and elevators.
An aggregate skip in a concrete batching plant is not automatically governed by the same rules.
For skip hoist maintenance, use:
- the equipment manufacturer’s manual;
- the applicable local machinery and lifting regulations;
- the plant’s risk assessment;
- inspection requirements established for the actual equipment category.
This avoids using an inspection interval intended for a different type of hoisting equipment.
After Major Repair, Recheck the Complete Travel Cycle
If ropes, brakes, drive components, guide parts or limit devices have been replaced, the plant should verify the hoist before normal production resumes.
يفحص:
- empty travel;
- loaded travel where approved;
- bottom position;
- top position;
- deceleration;
- braking;
- limit protection;
- alarm logic.
The test method should follow the manufacturer’s commissioning procedure.
Keep a Maintenance History by Component
| Record field | لماذا يهم |
|---|---|
| Rope inspection | Shows wear progression |
| Travel time | Can reveal increasing resistance |
| Motor current | Supports load and drag diagnosis |
| Brake service | Tracks adjustment history |
| Limit-switch replacement | Shows recurring position faults |
| Guide repair | Identifies alignment problem areas |
Skip hoist maintenance becomes more predictive when repeated faults are analyzed as trends.
Build Daily, Weekly and Planned-Shutdown Checks from the Manual
A practical inspection program can separate:
- operator observations during normal production;
- routine external inspections;
- planned shutdown inspections;
- manufacturer-required periodic inspections.
Do not invent one universal daily or monthly interval for every component.
The actual schedule should follow the supplied equipment documentation, duty cycle and applicable regulations.
What Should Buyers Ask Before Ordering a Skip-Hoist Plant?
Maintenance access should be considered during plant selection.
يسأل:
- What type of rope system is used?
- How are the two ropes synchronized?
- Where are the limit protections located?
- How is the raised skip mechanically secured for maintenance?
- Can the drum and brake be inspected safely?
- How are guide components accessed?
- Which spare parts are considered critical?
لدينا حلول إنتاج الخرسانة can compare skip-hoist and belt-fed plants against site, production and maintenance requirements.
What Should Operators Send for Technical Troubleshooting?
A useful skip hoist maintenance review needs operating evidence.
يقدم:
- plant model;
- skip load;
- fault description;
- alarm history;
- وقت السفر؛;
- motor current where available;
- photos of rope and guide condition;
- recent maintenance history;
- whether the problem occurs loaded, empty or both.
Send your plant model, symptoms and operating records through our صفحة الاتصال للمراجعة الفنية.
خاتمة
Skip hoist maintenance should cover the complete lifting system: hopper, dual ropes, drum, drive, brake, guides, limit protections, electrical signals and loading/discharge positions.
The strongest inspection strategy combines safe operating observations with planned shutdown checks and condition trends such as travel time, motor current and recurring alarm history.
Do not treat rope wear, tracking, braking or limit-switch faults as isolated issues. A skip hoist is a connected mechanical and control system, and reliable aggregate lifting depends on every part of that system working together.
الأسئلة الشائعة
What should be checked during skip hoist maintenance?
Inspect the hopper, wire ropes, rope terminations, drum, guides, rollers, drive motor, gearbox, brake, limit switches, loading position, discharge position and safety systems.
How often should skip hoist wire ropes be inspected?
Use the inspection frequency specified by the equipment manufacturer and the applicable local regulation for the actual equipment category. Operating duty and condition history can justify additional checks.
Why does a skip hoist stop at the wrong position?
Possible causes include limit-switch movement, brake behavior, rope stretch, guide problems, drive-control issues or mechanical obstruction. The entire travel system should be checked.
Can one damaged rope be replaced without checking the other rope?
In a synchronized dual-rope system, both ropes and their attachment, tension and winding conditions should be reviewed together. Replacement requirements should follow the manufacturer’s procedure.
What information is useful when troubleshooting a skip hoist?
Provide the plant model, load condition, alarm history, travel time, motor current, rope and guide photos and recent maintenance records.