Inhaltsverzeichnis
Batching plant selection for a two-shift operation starts with the production pattern across both shifts. A plant that completes a short peak comfortably may still lose output when aggregate replenishment, cement delivery, cleaning and maintenance have to fit into a much longer operating day. The purchasing brief should describe sustained demand and the periods available to restore equipment and material stocks.
The useful question is how much accepted concrete can reach the required destinations over the planned operating period. Rated hourly output is one input. Material availability, the actual batch cycle, truck or casting-line readiness and planned interruptions determine whether that rating is relevant to the proposed business. This guide explains the information needed to compare configurations for that duty.
Base batching plant selection on both shifts
Record the required products, delivery windows and expected production sequence for each shift. Batching plant selection should distinguish a steady second shift from a short extension used only during a large order. A schedule with several changing recipes and interrupted deliveries is different from a continuous run of one established concrete mixture.
Provide an hourly demand profile where practical, identifying firm requirements and planning assumptions. Do not divide the daily volume by the nominal shift length and treat the result as the whole design duty. That average can conceal concentrated demand and long periods when the plant is waiting for a destination rather than producing concrete.
Identify which downstream resources work during both shifts. A precast transport system, laboratory or dispatch fleet may have a different timetable from the mixer. Include their availability in the review. If a destination stops early, extra plant capacity cannot by itself turn the remaining operating hours into useful output.
Use the complete demonstrated cycle
Separate weighing, ingredient transfer, mixing, discharge and readiness for the following batch. Some operations can overlap, while others depend on a shared route becoming available. Batching plant selection should use the cycle for the intended product and configuration, with the supplier stating the conditions behind an output estimate.
An illustrative calculation shows the difference between running time and scheduled time. If a demonstrated route delivers an accepted batch every two minutes, there are thirty cycles in an uninterrupted hour. That arithmetic is not a Yunguan performance claim and does not include material shortages, cleaning or downstream waiting. Replace the example with measured or contractually defined inputs for the actual project.
Keep rejected or held production separate from accepted output. A control-system count can include events that did not result in usable concrete at the destination. The acceptance method should define what is counted and where it is measured, so each supplier is evaluated against the same production requirement.
Check replenishment while production continues
Review aggregate-bin capacity, loader movement, cement supply and water availability over the longest required run. Batching plant selection for two shifts needs a credible replenishment plan. A material buffer that supports a morning peak may not cover a supplier delivery interruption later in the day.
Record the usable capacity of each store rather than relying only on its nominal volume. Different materials, residual stocks and operating restrictions can affect the available buffer. Ask the supplier how the proposed arrangement supports receiving and feeding simultaneously, and identify any activity that requires the production route to stop.
Include receiving access and traffic. Longer production hours can overlap with bulk deliveries, maintenance vehicles and shift changes. The site layout should keep the relevant routes workable. Compare replenishment requirements against the actual loader and delivery arrangements instead of assuming that a second shift simply doubles material availability.
Reserve realistic maintenance and cleaning windows
List the tasks required by the equipment instructions and the factory's operating procedure. Assign a time and resource to each relevant activity. Batching plant selection should account for inspections, cleaning, lubrication and replacement planning before committing the entire day to production.
Distinguish tasks performed outside the active production route from those requiring equipment shutdown and controlled access. The authorized maintenance team should define those boundaries. An optimistic schedule should not depend on completing shutdown work while the equipment continues to operate.
Ask how service access changes between proposed configurations. A higher-output arrangement may have more conveying equipment or elevated components to inspect. A compact arrangement may constrain replacement access. Compare the complete maintenance task with the layout rather than ranking proposals only by the number of installed machines.
Review the consequence of a single interruption
Identify the equipment whose unavailability stops the required product route. Batching plant selection should connect contingency planning with the commercial consequence of lost output. A small buffer, alternative material route or defined backup supply may matter more than extra nominal mixing capacity.
Evaluate the expected response using the owner's maintenance resources and supplier support arrangements. Ask which parts can be held locally, which require configuration and which need specialist assistance. Avoid describing standby capacity as available until the interfaces, material supply and operating procedure have been checked.
Test the recovery process where appropriate during commissioning. The plant should preserve the status of interrupted batches and identify material that needs review. A fast electrical restart is not a complete production recovery if the team cannot establish whether the last batch was completed, held or rejected.
Compare proposals on a common duty sheet
| Review item | Information supplied by the buyer | Supplier response to request |
|---|---|---|
| Shift profile | Products, delivery windows and required periods | Output basis for each relevant operating condition |
| Batch cycle | Intended mixtures and batch range | Cycle boundaries and overlap assumptions |
| Material supply | Receiving frequency and available site equipment | Usable buffers and replenishment interfaces |
| Planned interruptions | Required cleaning and maintenance activities | Access, resources and shutdown assumptions |
| Downstream route | Dispatch or casting constraints | Discharge and transport compatibility |
| Recovery | Consequence of a stopped route | Fault response, records and return-to-service scope |
Use the same duty sheet for every offer. Batching plant selection becomes difficult when one proposal assumes continuous material supply and another includes replenishment stops. Require exclusions and assumptions to remain visible, so a lower quoted price is not confused with a more complete production solution.
Plan the second-shift handover
Define which information passes from one shift to the next: material stocks, active recipe versions, held batches, equipment issues and maintenance work. The operation needs a consistent record rather than a verbal instruction that the plant was running normally when the first team left.
Batching plant selection should include the control and reporting features that make this handover practical. Ask how operators retrieve unresolved alarms and production exceptions, and how the next team sees the status of material availability. A useful screen or export should support the actual handover procedure, not add records that nobody reviews.
Consider the availability of quality and maintenance support during the second shift. Define who can authorize recipe changes, release held production and respond to a fault. Equipment capability and organizational readiness need to align before the site commits to the new operating pattern.
Demonstrate sustained operation during acceptance
Agree a representative test covering the intended sequence, material replenishment and destination route. The buyer and supplier should define the duration and conditions appropriate to the contractual duty. A short demonstration can verify some functions, but its limits should be stated clearly.
Record accepted output, cycle observations, waiting causes and relevant material conditions. Batching plant selection should be supported by evidence showing which part of the system limits production. If the test exposes a supply or downstream constraint, retain that finding rather than removing the affected period from the results without explanation.
Close issues against the agreed acceptance criteria. Record the correction and the verification performed. Where the actual project duty cannot be reproduced at commissioning, identify the remaining obligation and how it will be evaluated under representative operation.
Send the operating profile with the equipment inquiry
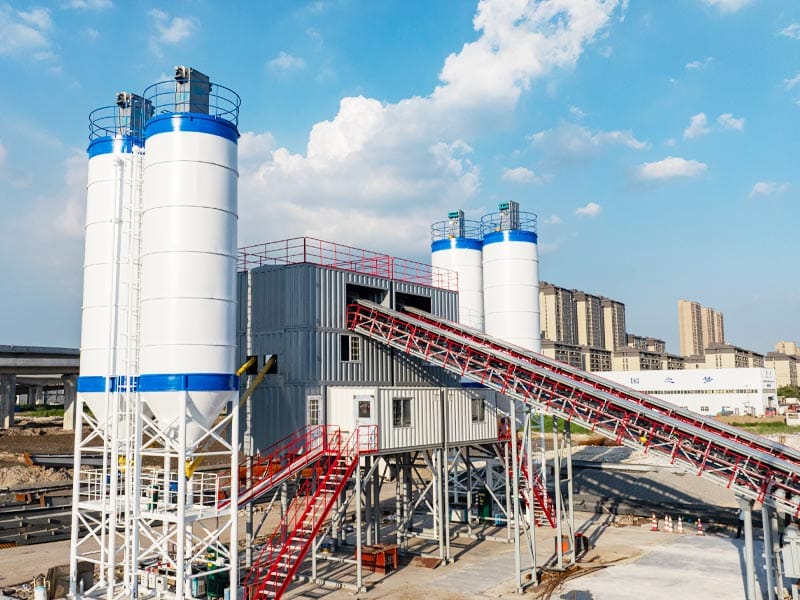
Review Yunguan's Überkopfbandbetonmischanlage und side-mounted belt arrangement against the site and shift profile. Provide the product range, planned operating hours, material deliveries and destination information. Ask the supplier to separate rated capacity from the conditions supporting sustained accepted output.
For background on a production-facility review, see the NRMCA plant inspection process. Use the project's own approved quality requirements and the proposed equipment documentation for the actual acceptance decision.
Send a representative two-shift demand profile through the form below. Include planned stops and known material constraints so the configuration discussion addresses the complete operating day.
Häufig gestellte Fragen
Does two-shift batching plant selection automatically require a larger mixer?
No. Batching plant selection should start with the demand profile and identified constraint. Material replenishment, maintenance or the downstream route may limit useful output before mixer size does.
Is daily volume divided by operating hours a sufficient duty figure?
It is a useful average, but it can hide concentrated demand and interruptions. Provide the production sequence and required delivery windows as well.
What is the right buffer size for two shifts?
Calculate it from the relevant material demand, replenishment pattern and credible interruption. Ask the supplier to identify usable storage under the proposed arrangement rather than applying a universal duration.
What should the acceptance trial record?
Record the defined accepted output, complete cycle, replenishment, waiting causes and production conditions. The test should make its coverage and limitations clear.
What information helps compare plant proposals fairly?
Use a common duty sheet covering both shifts, products, material supply, planned stops and destinations. Require each supplier to identify the assumptions behind its proposed output.