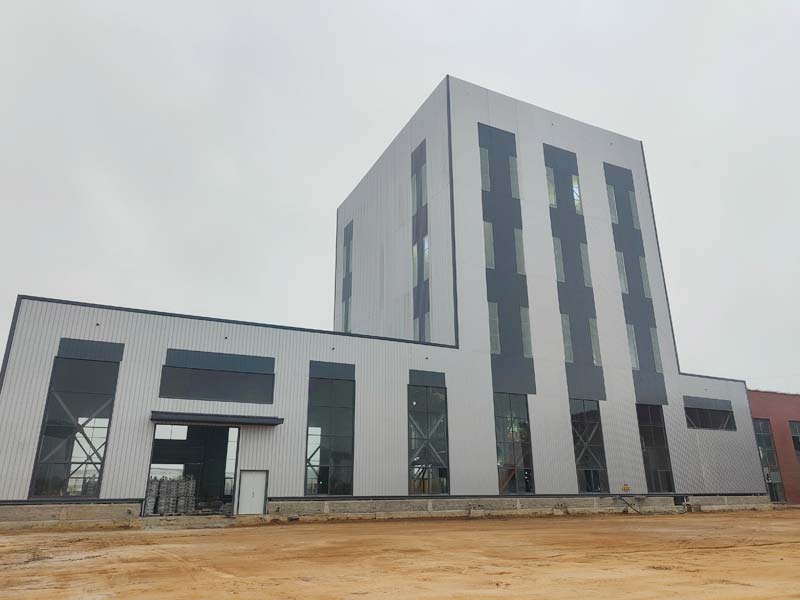
Dry mortar plant layout should follow the complete material path, not just the position of the mixer. Sand, cementitious powders, fillers, additives and finished mortar all need storage, weighing, transfer and access space. If these routes conflict, a plant with adequate mixer capacity can still lose production time through long transfers, blocked aisles, packaging bottlenecks or difficult maintenance.
For buyers, the best way to review a layout is to follow one batch from raw material intake to finished-product dispatch. Every transfer should have a defined function, enough capacity and practical access for cleaning and service.
Bizim kuru harç üretim çözümleri include tower, step and workshop configurations. A tower layout concentrates material vertically, a step layout combines elevated stages with mechanical transfers, and a workshop layout distributes the line more horizontally inside an industrial building. This guide explains how dry mortar plant layout should be planned around actual process flow.
What Should a Dry Mortar Plant Layout Include?
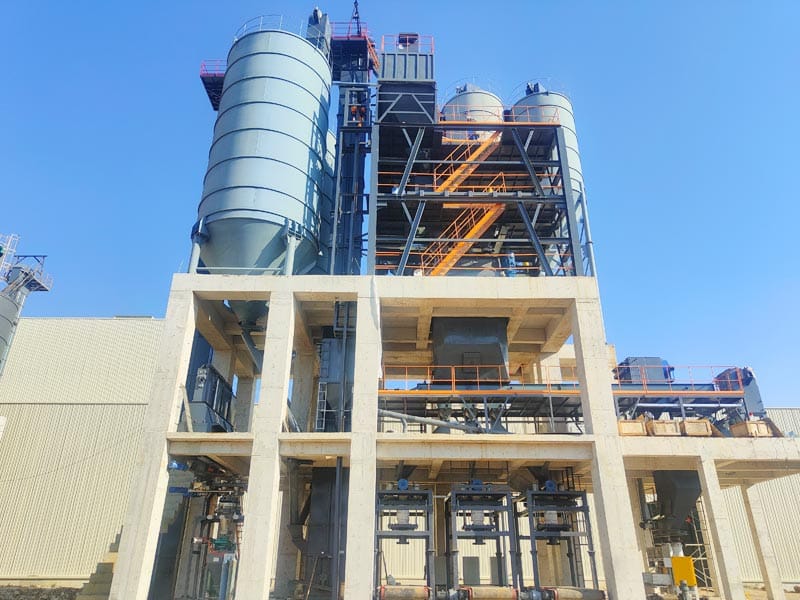
A complete dry mortar plant layout should show more than equipment footprints. It should identify where every material enters, where it is stored, how it is weighed, where it is mixed and how the finished product leaves the plant.
Typical zones include:
- sand receiving and preparation;
- sand storage;
- cement, filler and powder silos;
- bag-dump or additive handling;
- batching and weighing;
- karıştırma;
- finished-product buffer;
- bagging or bulk loading;
- pallet or finished-goods storage;
- toz toplama;
- bakım erişimi;
- quality-control sampling;
- vehicle circulation.
Dry mortar plant layout works best when these zones support one continuous production sequence rather than forcing material to move backward through the plant.
Start with Raw Material Intake
The first design question is how each raw material arrives.
| Raw material | Typical receiving question | Layout impact |
|---|---|---|
| Sand | Does it arrive dry, wet, graded or ungraded? | Determines whether drying, screening or classification is needed. |
| Cement and fillers | Are they delivered by bulk tanker or bags? | Determines silo filling access or bag-dump space. |
| Additives | Are they in small bags, big bags or bulk containers? | Defines micro-dosing and operator handling zones. |
| Packaging materials | How are empty bags stored and moved? | Requires dry storage close to the packing area. |
A dry mortar plant layout should separate bulk tanker access, sand delivery and finished-product dispatch where possible. Receiving traffic should not repeatedly block the packaging or forklift area.
Dry Sand Should Enter the Storage System in a Controlled Condition
If wet sand is delivered, the plant may need drying and cooling before the material enters dry storage.
If dry graded sand is purchased, those stages may be unnecessary.
Dry mortar plant layout should therefore define the process boundary before equipment is positioned.
For an integrated manufactured-sand project, our manufactured sand and special mortar plant can connect sand preparation and classification directly with downstream mortar production.
The key point is to avoid duplicating equipment. If the upstream sand section already provides approved dry fractions, the mortar plant should receive those fractions directly into the correct storage bins.
Sand Storage Should Match the Product Portfolio
One sand bin may be enough for a simple product range, but a special mortar factory may need several fractions.
Tile adhesive, masonry mortar, self-leveling mortar and repair mortar can require different fine-aggregate distributions.
For dry mortar plant layout, determine:
- kum fraksiyonlarının sayısı;
- daily consumption of each fraction;
- replenishment frequency;
- maximum storage time;
- whether fractions need to be blended.
Bizim harç kılavuzu için ince kum explains why one sand-size range should not automatically be applied to every mortar product.
Powder Silo Position Should Support Tanker Access
Cement and mineral fillers are often stored in silos and delivered by tanker.
Dry mortar plant layout should give tankers enough room to enter, connect to filling lines, unload and leave without blocking finished-goods traffic.
Kontrol:
- tanker turning space;
- filling-pipe location;
- operatör erişimi;
- dust-collector access;
- clearance around silo supports;
- future silo expansion.
The powder-storage zone should also remain accessible for level-sensor, valve and dust-collector maintenance.
Micro-Additive Handling Needs a Separate Clean Zone
Low-dose additives should not be treated like bulk sand or cement.
These materials may arrive in bags and require manual bag opening, small-hopper storage or dedicated micro-dosing equipment.
Dry mortar plant layout should provide enough space for:
- identified additive storage;
- çanta açma;
- toz emme;
- tartı;
- safe operator access;
- empty-bag handling;
- cleaning between products.
This zone should be arranged to reduce the risk of adding the wrong ingredient to the wrong recipe.
Batching Equipment Should Follow Material Groups
Sand, bulk powders and micro-additives often require different weighing ranges.
Dry mortar plant layout should position the weighing systems so ingredients can be prepared efficiently without unnecessary cross-transfer.
For example:
- sand can use dedicated aggregate scales;
- cement and fillers can use powder scales;
- small additives can use micro-dosing systems.
Bizim kuru harç tartım doğruluk kılavuzu explains why small-dose ingredients should not simply share the same measuring range as bulk materials.
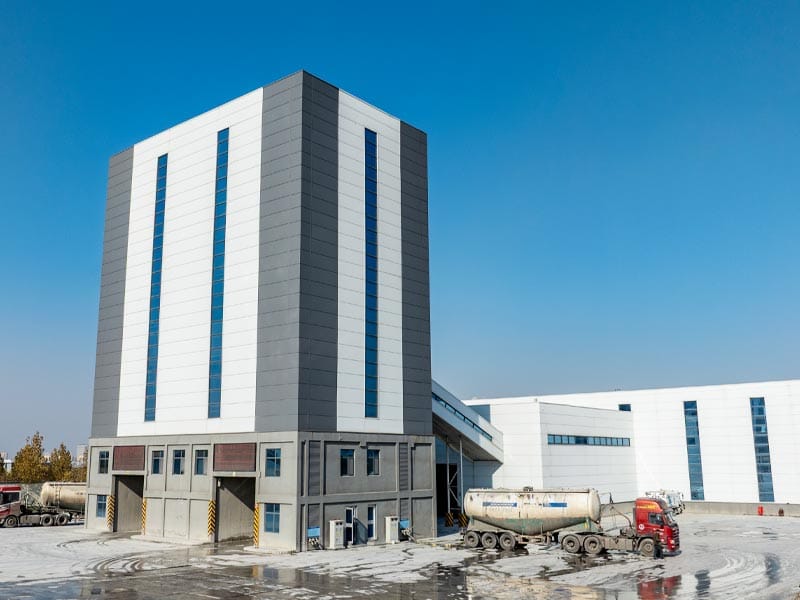
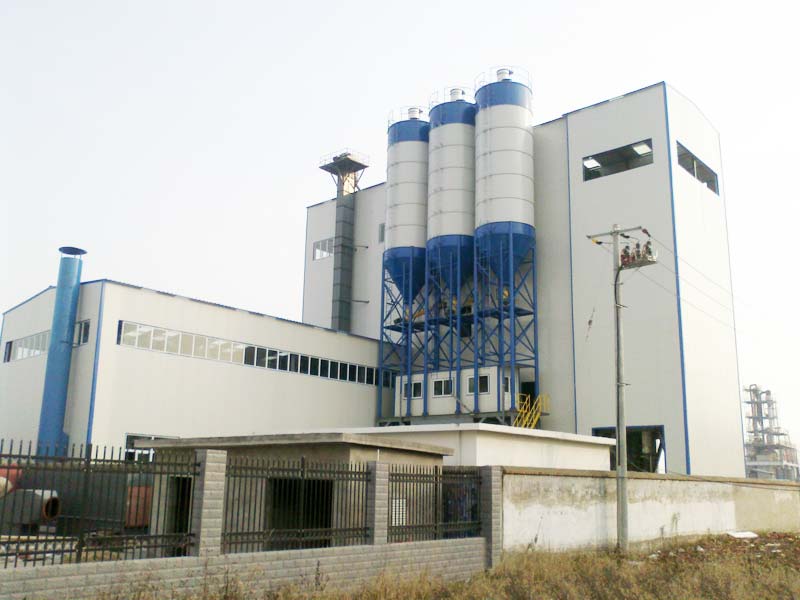
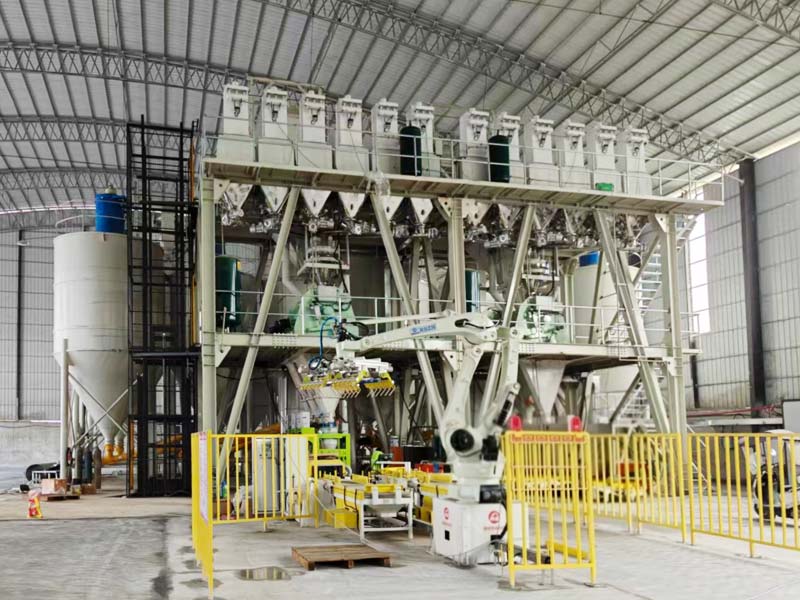
Tower Layouts Use Vertical Gravity Flow
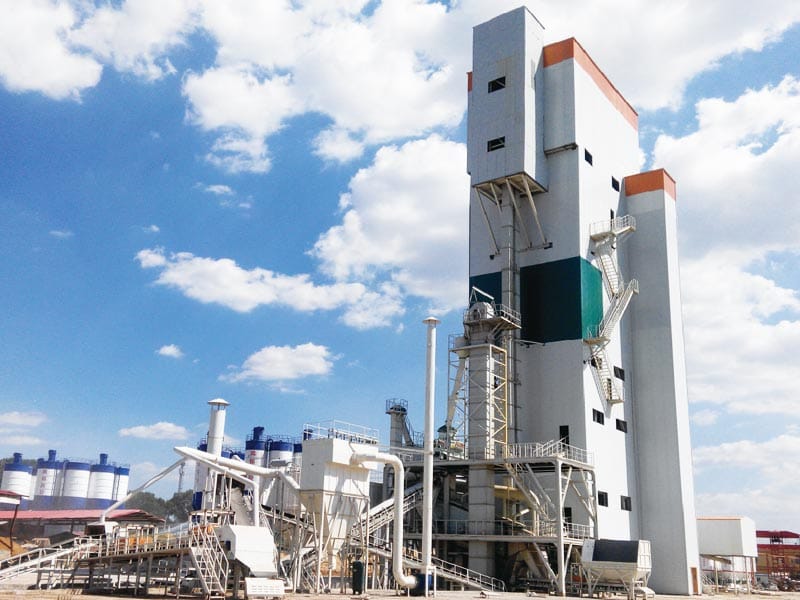
A tower-type dry mortar plant places major storage, batching, mixing and downstream handling stages in a vertically integrated arrangement.
Material enters from higher levels and moves downward through several stages by gravity.
This can reduce the number of mechanical transfers and centralize the process.
For dry mortar plant layout, a tower configuration requires careful review of:
- total structure height;
- foundation and structural loads;
- elevated maintenance access;
- silo replenishment;
- vertical material routes;
- packaging and dispatch beneath the main process.
Bizim kule tipi kuru harç karıştırma tesisi uses this vertically integrated concept. The final configuration still needs to be matched to the real product mix and site.
Step Layouts Balance Height with Mechanical Transfer
A step-type arrangement distributes major process stages across different elevations rather than concentrating everything in one vertical tower.
Some material moves downward by gravity while other material is transferred mechanically between stages.
Dry mortar plant layout for a step configuration should show:
- each elevation;
- which transfer uses gravity;
- which transfer uses screw or other conveying;
- intermediate hopper capacity;
- maintenance routes;
- space for future modifications.
Do not assume every step plant has the same number of transfers or the same capacity. Follow the proposed process diagram for the actual project.
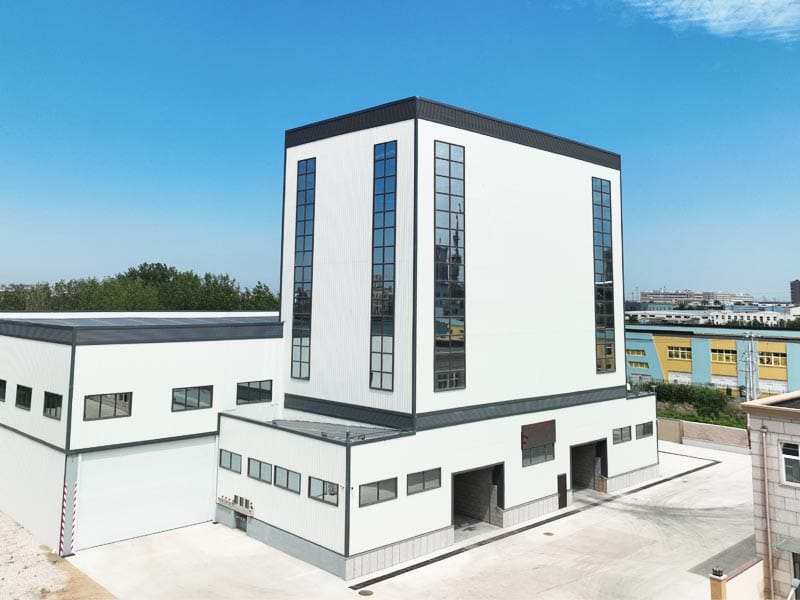
Workshop Layouts Use More Horizontal Space
A workshop-type dry mortar plant distributes core equipment on the same or similar floor level and connects stages with screw conveyors.
Bizim atölye tipi kuru harç karıştırma tesisi is designed for installation inside an industrial workshop and supports horizontally expanded material flow.
This layout can be useful for small-batch and special mortar production because equipment remains relatively accessible.
However, dry mortar plant layout inside a workshop needs to account for:
- usable clear height;
- columns;
- floor loading;
- door openings;
- screw-conveyor withdrawal space;
- packing and pallet traffic;
- dust-control ducting.
The mixer fitting inside the building does not prove the complete line fits.
Conveyors Need Maintenance Space, Not Just Operating Space
Screw conveyors, bucket elevators and other transfer equipment occupy more than their centerline.
Dry mortar plant layout should reserve space to remove screws, service bearings, open inspection covers and replace drives.
Kontrol:
- withdrawal direction;
- motor access;
- destek yapıları;
- inspection doors;
- cleanout locations;
- safe access platforms.
A conveyor that fits between two walls may still be impossible to service if there is no room to remove its internal screw or shaft.
The Mixer Should Sit at the Center of the Production Logic
The mixer is where all ingredient routes converge.
Dry mortar plant layout should therefore minimize unnecessary waiting before and after mixing.
Upstream weighing systems should be able to prepare the next batch while the current batch is mixing where the process allows it.
Downstream equipment should be ready to accept the finished batch without forcing the mixer to remain full.
This makes intermediate hoppers and finished-product buffers important design tools.
They can decouple process stages, but only if their usable volume matches the production cycle.
Finished-Product Buffers Should Prevent Packaging from Stopping the Mixer
Packaging often operates at a different rhythm from mixing.
A finished-product hopper can provide short-term buffering between the mixer and packer.
For dry mortar plant layout, check:
- usable buffer volume;
- number of products sharing the buffer;
- segregation risk;
- erişimi temizlemek;
- packer feed method;
- maximum acceptable storage time.
A buffer cannot solve a permanent packaging bottleneck. If the mixer continuously produces faster than the packer, the buffer will eventually fill.
Packaging Needs Its Own Production Zone
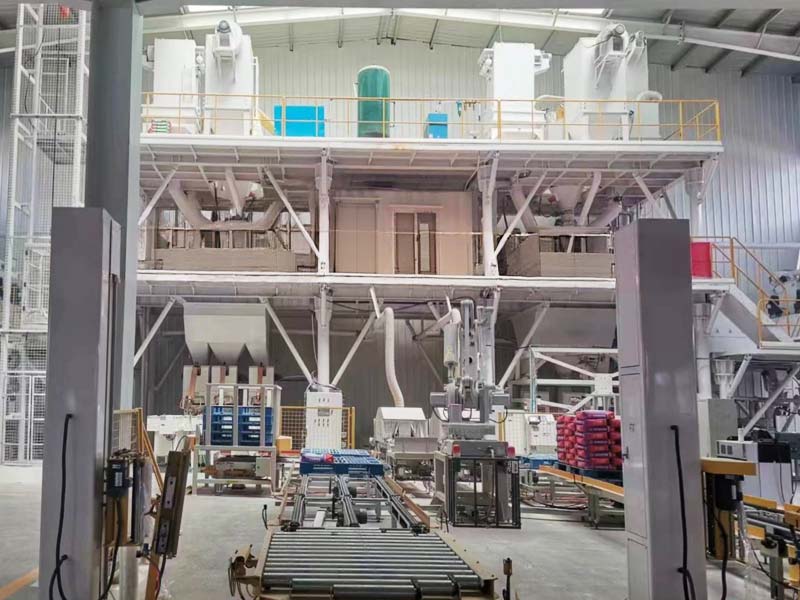
The packing area needs more space than the bagging machine itself.
Dry mortar plant layout should include:
- empty-bag storage;
- packer access;
- finished-bag conveyor;
- checkweighing where required;
- sealing;
- palletizing;
- forklift lanes;
- finished-goods staging.
Bizim harç çantası ağırlık değişimi kılavuzu explains why packer stability depends on product flow, hopper condition and bag handling as well as the weighing system.
Bulk Dispatch Should Be Separated from Bagged-Goods Traffic
Some dry mortar plants deliver both bags and bulk finished product.
If bulk loading is included, the dry mortar plant layout should define a separate vehicle position where tanker or silo-truck loading can occur safely.
Check whether bulk-loading vehicles would block:
- bagged-product forklifts;
- raw-material tankers;
- sand delivery;
- bakım erişimi;
- emergency routes.
Bulk loading can bypass the packaging line, but it creates its own dispatch interface.
Finished-Goods Storage Should Match Dispatch Rhythm
A plant can produce more bags than the warehouse can absorb.
Dry mortar plant layout should therefore include enough finished-product staging for the real shipping schedule.
Şunu düşünün:
- daily packaged output;
- pallet size;
- stacking rules;
- forklift routes;
- truck loading pattern;
- product separation;
- warehouse humidity control.
If several mortar products share one warehouse, clearly separated storage zones reduce dispatch errors.
Dust Collection Should Follow the Material Transfer Points
Dry mortar production handles fine powders at many stages.
Toz şu durumlarda üretilebilir:
- silo dolumu;
- çanta açma;
- tartı;
- mikser şarjı;
- karıştırıcı deşarjı;
- paketleme.
Dry mortar plant layout should place dust-capture points close to these sources and leave room for filter inspection and collected-material handling.
Birleşik Krallık Sağlık ve Güvenlik İdaresi yerel egzoz havalandırma kılavuzu emphasizes capturing contaminants close to the source and commissioning systems under real operating conditions.
Dust-control ducting should be part of the layout drawing, not added after equipment positions are fixed.
Separate Personnel Routes from Forklifts and Delivery Trucks
Dry mortar plants can have several vehicle types operating at the same time:
- raw-material tankers;
- sand trucks;
- forkliftler;
- finished-goods trucks;
- maintenance vehicles.
Dry mortar plant layout should reduce unnecessary crossings between these vehicles and personnel.
Mark:
- pedestrian walkways;
- forklift lanes;
- truck routes;
- emergency exits;
- maintenance access.
A plant with efficient material flow can still be difficult to operate if logistics routes compete for the same narrow aisle.
Plan Quality-Control Sampling Points
Quality teams need access to raw materials and finished product without stopping production unnecessarily.
Dry mortar plant layout should provide practical sampling locations for:
- sand;
- powders;
- additives;
- mixed dry mortar;
- finished bags.
Samples should be identifiable and linked to production records.
Locating the laboratory near the process can shorten response time, but it should be protected from excessive dust and traffic.
Cleaning and Product Changeover Need Physical Space
Multi-product mortar plants need to clean or purge equipment between selected recipes.
Dry mortar plant layout should therefore allow access to:
- micro-additive feeders;
- tartım hazneleri;
- conveyors;
- mixer inspection points;
- finished-product buffers;
- paketleyiciler.
Bizim dry mortar plant maintenance guide explains why cleaning and product readiness are part of practical plant availability.
A line that cannot be cleaned efficiently may lose more production time during changeovers than expected.
Future Expansion Should Be Drawn on the Initial Layout
Dry mortar plants often expand by adding:
- another powder silo;
- another sand fraction;
- micro-dosing equipment;
- a second packer;
- bulk loading;
- manufactured-sand preparation.
Dry mortar plant layout should reserve realistic expansion zones before the initial plant fills the site.
Also leave spare utility and control capacity where future growth is likely.
Horizontal expansion is particularly relevant to workshop configurations, while tower and step plants may need future structural provisions.
Review the Layout by Following One Complete Batch
Before approving the drawing, follow one batch from raw material arrival to finished dispatch.
| Process stage | Layout question |
|---|---|
| Raw material intake | Can deliveries unload without blocking another critical route? |
| Storage | Are required materials separated and accessible? |
| Batching | Can major and micro ingredients reach the correct scales efficiently? |
| Karıştırma | Can the next batch be prepared while the current batch mixes? |
| Finished transfer | Can the mixer discharge without waiting for downstream equipment? |
| Ambalaj | Can the packing line match the production schedule? |
| Dispatch | Forkliftler ve kamyonlar, bitmiş ürünü emişe müdahale etmeden hareket ettirebilir mi? |
Bu sürecin gözden geçirilmesi, kuru harç tesisi düzenini bir ekipman çiziminden bir işletme planına dönüştürür.
Alıcılar Kuru Harç Tesisi Yerleşim İncelemesi İçin Ne Göndermeli?
Yararlı bir kuru harç tesisi yerleşim incelemesi, gerçek üretim ve saha bilgilerine ihtiyaç duyar.
Sağlamak:
- ürün türleri;
- gerekli üretim programı;
- kum fraksiyonları;
- toz malzemeler;
- katkı kategorileri;
- hammadde dağıtım yöntemleri;
- torba boyutları ve toplu sevkiyat ihtiyaçları;
- site veya atölye boyutları;
- bina yüksekliği ve sütunları;
- kamyon ve forklift rotaları;
- yardımcı lokasyonlar;
- gelecekteki genişleme planları.
Bu girdiler, bir kulenin, basamağın, atölyenin veya entegre kum ve harç düzenlemesinin projeye en iyi şekilde uyup uymadığını belirlemeye yardımcı olur.
Ürün yelpazenizi ve site çiziminizi bizim aracılığımızla gönderin i̇letişim sayfası projeye özel kuru harç tesisi yerleşim planı incelemesi için.
Sonuç
Kuru harç tesisi düzeni hammadde alımından bitmiş sevkıyata kadar komple malzeme yolunu takip etmelidir Depolama, tartım, taşıma, karıştırma, tamponlama, paketleme, toz kontrolü ve lojistik hepsi alan ve üretim süresi için rekabet eder.
Kule, basamak ve atölye düzenleri bu işlevleri farklı şekilde düzenler Doğru seçim ürün yelpazesine, saha yüksekliğine, transfer gereksinimlerine, bakım erişimine ve paketleme stratejisine bağlıdır.
Çizimi onaylamadan önce önerilen hattın tamamında bir parti izleyin. Her malzeme rotası, bakım görevi ve sevk hareketinin net bir yolu varsa, tesisin işletilmesi ve genişletilmesi daha kolay olacaktır.
SSS
Kuru harç tesisi düzenindeki ana alanlar nelerdir?
Ana alanlar normalde hammadde alma, kum ve toz depolama, katkı maddesi taşıma, tartma, karıştırma, bitmiş ürün tamponlama, paketleme veya toplu yükleme, toz toplama, bakım ve bitmiş ürün sevkıyatını içerir.
Kule, basamak ve atölye kuru harç düzenleri arasındaki fark nedir?
Kule tesisleri malzemeyi dikey olarak yoğunlaştırır ve daha fazla yerçekimi akışı kullanır.Adım tesisleri yükseltilmiş aşamaları mekanik transferle birleştirir.Atölye tesisleri ekipmanı daha yatay olarak dağıtır ve aşamalar arasında yaygın olarak vidalı konveyörler kullanır.
Kuru harç tesisi düzeninde ambalaj neden önemlidir?
Ambalaj aşağı akış darboğaz haline gelebilir.düzen bitmiş ürün tamponları, paketleyiciler, çanta taşıma, paletleme ve forklift trafiği için alana ihtiyaç duyar, böylece karıştırıcı tekrar tekrar beklemeye zorlanmaz.
Mevcut bir atölyenin içine kuru harç tesisi kurulabilir mi?
Evet, binaya bağlı olarak Düzeni tamamlamadan önce net yüksekliği, sütunları, zemin yüklemesini, kapı açıklıklarını, ekipman erişimini, vidalı konveyör çekme alanını, toz kontrolünü ve paketleme lojistiğini kontrol edin.
Kuru harç tesisi yerleşim incelemesi için hangi bilgilere ihtiyaç vardır?
Ürün türleri, üretim hedefleri, hammaddeler, teslimat yöntemleri, saha veya bina boyutları, paketleme gereksinimleri, araç rotaları, kamu hizmetleri ve gelecekteki genişleme planlarını sağlayın.