

Hopper bridging in dry mortar plants can stop material flow even when a storage bin still contains plenty of product. Fine sand, cement, fillers and additives can form a stable arch above the outlet, leaving the feeder starved while material remains suspended inside the hopper.
For plant teams, the problem is more serious than a temporary blockage. Bridging can cause unstable weighing, long batch cycles, sudden material surges, screw-conveyor starvation and repeated operator intervention. If the real cause is not understood, the same hopper may keep blocking even after the material is manually cleared.
لدينا مصنع خلط الملاط الجاف من نوع الورشة uses storage bins, screw conveyors and metering hoppers to move sand, powder and additives into the mixer, while step-type layouts combine gravity flow with mechanical conveying between platforms. This guide explains how hopper bridging in dry mortar plants should be investigated from both the material and equipment sides.
What Is Hopper Bridging in a Dry Mortar Plant?
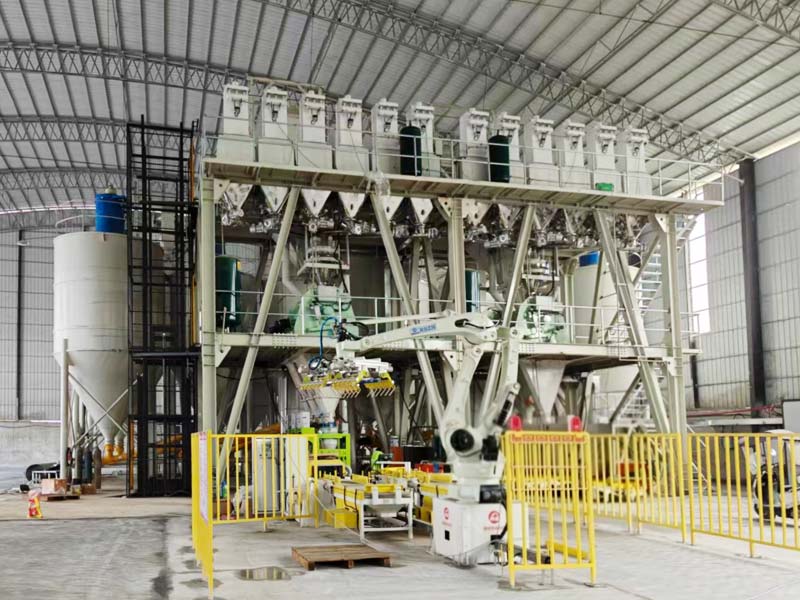
Hopper bridging occurs when bulk material forms a self-supporting arch across the outlet of a hopper or silo. Material below the bridge discharges, but the material above remains suspended.
Bridging is different from simply having an empty bin.
A bridged hopper may show:
- a low-level alarm even though material is visible above;
- no feed from the outlet;
- intermittent material flow;
- long feeder run times;
- sudden surges after a blockage collapses;
- repeated operator intervention.
For hopper bridging in dry mortar plants, the important question is why the material can support itself above the outlet.
Bridging and Ratholing Are Different Problems
Bridging blocks the entire hopper outlet. Ratholing creates a narrow flow channel through the material while a stagnant layer remains around the walls.
| Flow problem | What happens | Typical production symptom |
|---|---|---|
| Bridging | A stable arch forms above the outlet. | Flow stops completely. |
| Ratholing | A central channel empties while material remains along the walls. | Flow continues but usable capacity drops and discharge becomes unstable. |
| Caking | Material consolidates into hard lumps. | Feed becomes irregular or impossible after storage. |
| Flooding | A fine powder becomes aerated and flows too freely. | Unexpected surges or loss of feeder control. |
Hopper bridging in dry mortar plants should therefore not be used as a generic term for every poor-flow problem.
Fine Powders Can Form Cohesive Bridges
Cement, mineral fillers and some additives can behave as cohesive powders.
These materials can develop enough internal strength to span the outlet when they are compressed or stored for a period of time.
Factors that can increase cohesive behavior include:
- very fine particle size;
- moisture;
- long storage time;
- consolidation pressure;
- electrostatic effects;
- surface chemistry.
For hopper bridging in dry mortar plants, a powder that flows well during one trial may behave differently after several hours or days of storage.
That is why plant design should use representative stored material rather than only freshly opened laboratory samples.
Fine Sand Can Bridge for Different Reasons
Fine sand can bridge even when it is less cohesive than cement powder.
Particle shape, moisture, fines content and hopper outlet size all matter.
Manufactured sand may contain angular particles and fine stone powder. Natural sand may contain varying moisture and fine contamination. Either material can become difficult to discharge if the actual bulk behavior does not match the hopper design.
لدينا fine sand for mortar guide explains why particle-size distribution and powder content should be controlled for the mortar product. Those same properties also affect bulk flow through storage equipment.
Moisture Is a Major Bridging Risk
Dry mortar production depends on dry raw materials, and excess moisture can change powder and sand flow dramatically.
Moisture can create liquid bridges between particles, increase cohesion and cause material to stick to hopper walls.
For hopper bridging in dry mortar plants, check whether the problem becomes worse:
- during rainy seasons;
- after a dryer upset;
- after long storage;
- with one specific sand source;
- when warm material cools and condensation forms.
If a hopper bridges only when material moisture rises, changing the hopper vibrator may treat the symptom without solving the upstream material problem.
Hopper Outlet Size Can Be More Important Than Hopper Volume
A large hopper can still bridge if its outlet is too small for the material. In practice, hopper bridging in dry mortar plants often begins where outlet geometry and material strength are mismatched.
The outlet has to be large enough that the material cannot form a stable arch across it under the actual stress condition.
For hopper bridging in dry mortar plants, buyers should avoid sizing outlets from throughput alone.
مراجعة:
- material cohesion;
- particle size;
- particle shape;
- wall friction;
- hopper angle;
- expected consolidation.
A feeder may be able to handle the required tonnes per hour, but that does not guarantee the hopper above it can deliver material continuously.
Wall Angle and Wall Friction Control How Material Moves
Material sliding along the hopper wall experiences friction.
If the wall is too shallow or the material has high wall friction, a stagnant region can develop and support bridging or ratholing.
Hopper bridging in dry mortar plants should therefore be reviewed with the actual wall material and bulk solid.
Changing only the hopper angle without considering surface condition may not solve the problem.
Check:
- wall material;
- surface roughness;
- welds and transitions;
- liners;
- corrosion or buildup;
- hopper geometry.
A smooth hopper when new can behave differently after residue, wear or corrosion changes the wall surface.
Mass Flow and Funnel Flow Behave Differently
Bulk solids can discharge in different flow patterns.
In mass flow, material moves throughout most of the hopper as discharge occurs. In funnel flow, a central channel moves while material near the walls can remain stagnant.
For hopper bridging in dry mortar plants, the choice between these behaviors matters because stagnant zones can:
- hold old product;
- increase caking;
- create recipe contamination;
- reduce usable storage;
- make first-in/first-out behavior difficult.
The correct hopper design depends on material characteristics and process goals. Not every dry mortar hopper needs the same flow pattern, but the intended behavior should be understood before the equipment is finalized.
Transitions and Dead Corners Can Start a Flow Problem
A hopper can have an adequate outlet and still develop poor flow around internal ledges, abrupt transitions or poorly designed connections. Hopper bridging in dry mortar plants can therefore originate above the nominal outlet itself.
For hopper bridging in dry mortar plants, inspect:
- bin-to-screw transitions;
- gate frames;
- flanges;
- internal supports;
- weld beads;
- inspection-door frames.
Material can accumulate around these features and gradually narrow the effective flow path.
If a hopper worked when new but began bridging later, inspect for buildup before changing the control settings.
Screw Conveyors Cannot Fix a Starved Hopper
Workshop-type dry mortar lines often use screw conveyors to transfer sand, powders and additives between storage and metering stages.
A screw conveyor can only move material that reaches its inlet.
If the hopper above the screw is bridged, the screw may continue rotating with little or no material.
This can create:
- long filling times;
- weighing timeouts;
- underweight hoppers;
- unstable screw loading;
- sudden surge when the bridge collapses.
Hopper bridging in dry mortar plants should therefore be diagnosed upstream of the screw before the screw speed is changed.
Changing Screw Speed Can Make the Symptom Worse
If operators see low material flow, they may increase screw speed.
That can empty the small amount of material available at the hopper outlet even faster and make the starvation cycle more severe.
For hopper bridging in dry mortar plants, compare:
- hopper level;
- screw motor load;
- feeder speed;
- weighing rate;
- time between flow interruptions.
If the screw motor load repeatedly drops before the weighing rate falls, the problem may be material supply rather than conveyor capacity.
Bridging Can Destabilize Weighing Accuracy
A bridged hopper can interrupt the feed into a weighing hopper.
The control system may wait, time out or receive a sudden surge after the arch collapses.
This makes accurate fine dosing difficult.
For hopper bridging in dry mortar plants, unstable weighing can appear as:
- slow approach to target;
- underweight batches;
- overshoot after sudden flow resumes;
- large variation in dosing time;
- frequent manual intervention.
لدينا dry mortar weighing accuracy guide explains why feeding behavior and scale performance need to be evaluated separately.
Small Additive Hoppers Can Be Especially Sensitive
Micro-additive systems handle small quantities, and their hoppers may be much smaller than sand or cement bins.
Fine polymers, cellulose ether, pigments or other specialty ingredients can have poor flow properties.
Hopper bridging in dry mortar plants can therefore appear first in the micro-dosing section.
Check:
- material storage time;
- hopper outlet;
- feeder inlet;
- humidity exposure;
- bag-dump procedure;
- powder compaction after filling.
Do not assume that a small hopper is automatically less likely to bridge.
Finished-Product Hoppers Can Bridge Too
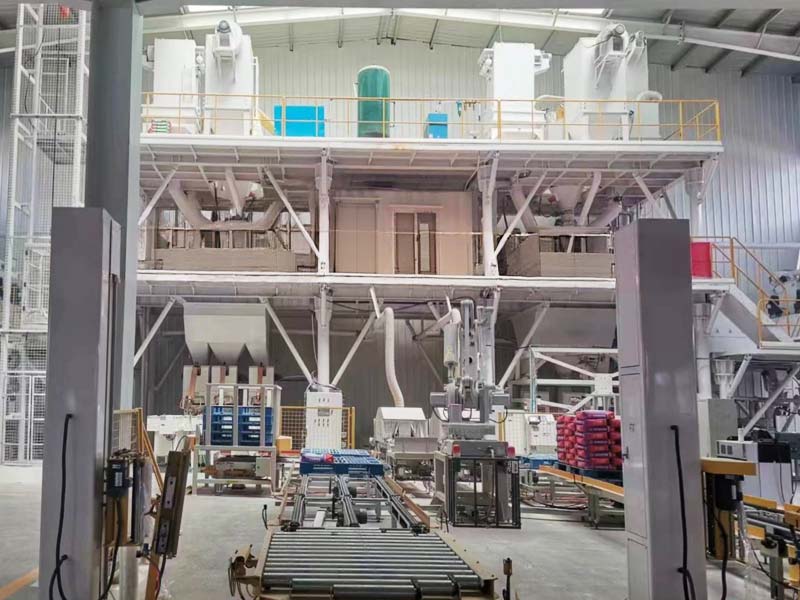
Bridging is not limited to raw materials.
Finished dry mortar can bridge above the packaging system, especially when the product is fine, cohesive or stored for too long before bagging.
This can create:
- packer starvation;
- unstable bag filling;
- long packaging cycles;
- sudden product surges;
- bag-weight variation.
لدينا mortar bag weight variation guide explains how unstable hopper feed can affect the packing line.
Dust Extraction Can Affect Very Fine Powder Flow
Dry mortar plants use dust collection around transfer, weighing and packaging points.
For very fine powders, uncontrolled pressure conditions can influence how material behaves near outlets and feeders.
Hopper bridging in dry mortar plants should therefore be checked with the dust system operating under its normal production condition.
The UK Health and Safety Executive’s local exhaust ventilation guidance emphasizes commissioning extraction systems under realistic operating conditions.
The goal is not to remove dust control. It is to make sure the ventilation arrangement and bulk-solids system are designed to work together.
Vibrators Are Flow Aids, Not Universal Solutions
External vibrators can help some materials flow, but they should not be treated as the automatic solution to every bridge.
Vibration can sometimes compact a cohesive powder more tightly or create unstable surges.
For hopper bridging in dry mortar plants, decide whether a vibrator is appropriate based on:
- material behavior;
- hopper geometry;
- mounting location;
- operating sequence;
- structural design.
Continuous uncontrolled vibration is different from a properly engineered flow-aid strategy.
Air Pads and Aeration Need Material-Specific Review
Air-assisted flow devices can be effective for some fine powders, but they also change the bulk state of the material.
Too much aeration can make some powders flood or feed too quickly.
For hopper bridging in dry mortar plants, confirm:
- whether the material responds well to aeration;
- air pressure and flow requirements;
- installation location;
- dust-control interaction;
- effect on weighing stability.
Do not apply air to every sand, powder or additive hopper with the same settings.
Manual Rodding and Hopper Entry Create Serious Safety Risks
Repeated manual clearing is a sign that the flow problem needs an engineering solution. Hopper bridging in dry mortar plants should be corrected through material and equipment review rather than normalized as routine operator work.
Workers should not place themselves beneath unstable stored material or enter a hopper to break a bridge without the required hazardous-energy and confined-space controls.
إدارة السلامة والصحة المهنية التحكم في معايير الطاقة الخطرة requires covered servicing activities to isolate hazardous energy where unexpected startup or stored-energy release could cause injury.
NIOSH has also documented engulfment hazards associated with bridged bulk materials in bins and silos. The exact regulatory requirements depend on the facility and task, but the engineering lesson is clear: do not make routine manual entry part of normal hopper operation.
Use Time-Based Production Data to Find Bridging
Hopper bridging in dry mortar plants can be detected through production trends before operators physically inspect the bin.
Track:
| Data point | What it can reveal |
|---|---|
| Feeder run time | Longer time can indicate reduced material flow |
| Weighing time | Large variation can indicate intermittent feed |
| Screw motor load | Low load can indicate starvation |
| Low-level alarms | Can reveal a false empty condition below a bridge |
| Operator interventions | Shows which hopper repeatedly needs attention |
If one hopper consistently has longer dosing times than similar hoppers, investigate material flow before increasing cycle allowances in the control system.
Changeover Can Reveal Hidden Stagnant Material
A hopper that appears to empty may still contain stagnant material along the walls.
When the plant switches products, this residue can enter a later batch and contaminate the next formulation.
For hopper bridging in dry mortar plants, check:
- whether the bin fully empties;
- whether material remains above the outlet;
- whether old product appears after a refill;
- whether cleaning access reaches stagnant zones.
This is especially important in multi-product special mortar lines.
لدينا workshop dry mortar plant guide explains why multi-product production should be planned together with access and changeover requirements.
Test Bulk Flow Before Finalizing Hopper Geometry
The best way to reduce bridging risk is to understand the real material before the hopper is fabricated.
Representative bulk-solids testing can help determine:
- cohesive strength;
- wall friction;
- bulk density;
- effect of consolidation;
- effect of moisture;
- likely flow pattern.
For hopper bridging in dry mortar plants, this information can be used to review outlet dimensions, wall angle and lining material.
Do not design a critical additive or fine-powder hopper only from material name. Two products both called “filler” can have very different flow behavior.
What Should Buyers Send for Hopper and Storage Design?
A useful bulk-material review needs more than the ingredient list.
يقدم:
- material name;
- particle-size distribution;
- bulk density;
- moisture or humidity sensitivity;
- normal storage time;
- required feed rate;
- minimum dosing rate;
- whether the material compacts during storage;
- existing flow problems if the material is already in use.
For fine powders and additives, samples may be needed for flow testing before the final hopper design is confirmed.
Send your raw-material list and process requirements through our صفحة الاتصال for a project-specific dry mortar line review.
خاتمة
Hopper bridging in dry mortar plants is a bulk-flow problem that can affect weighing, screw conveying, packaging and production stability. Fine powders, moist sand, small outlets, high wall friction, poor transitions and long storage can all contribute.
The most effective solution starts by separating bridging from ratholing, caking and feeder problems, then reviewing the actual material together with hopper geometry and downstream equipment.
Do not rely on repeated manual clearing as normal operation. Design storage and flow equipment around real material behavior so the dry mortar line can feed, weigh and package consistently.
الأسئلة الشائعة
What causes hopper bridging in dry mortar plants?
Common causes include cohesive fine powders, moisture, small outlets, high wall friction, shallow hopper geometry, long storage and material compaction. The exact cause depends on the material and hopper design.
What is the difference between bridging and ratholing?
Bridging creates an arch that blocks the outlet completely. Ratholing creates a narrow central flow channel while material remains stagnant along the hopper walls.
Can a screw conveyor solve hopper bridging?
No. A screw conveyor can only move material that reaches its inlet. If the hopper above it is bridged, increasing screw speed may make the starvation cycle worse.
Should I install a vibrator on every dry mortar hopper?
No. Vibrators are useful for some materials but can compact others or create sudden surges. The flow aid should be selected according to material behavior and hopper design.
How can hopper bridging be prevented during plant design?
Use representative material data or bulk-flow testing to review outlet size, wall angle, wall surface, storage time and feeder interface before fabrication. Design decisions should be based on the actual powder or sand being stored.


