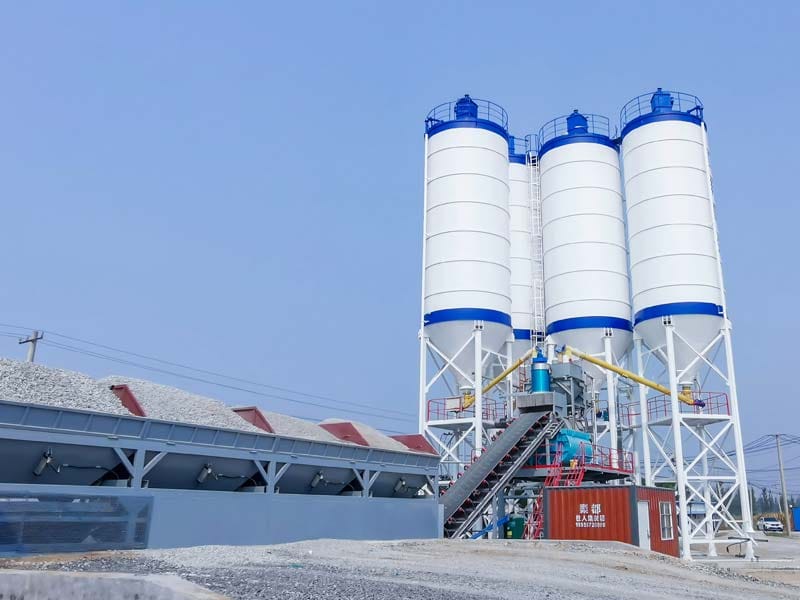
Toplu tesis bakımı ilk arızadan önce başlar - ve ideal olarak tesis satın alınmadan önce. Bir konveyörü incelemek, bir astarı değiştirmek ve bir tartım hunisini doğrulamak için yer bırakan bir düzen, bakım ekibine uygulanabilir bir başlangıç noktası sağlar.
Bizim yana monteli bant beton karıştırma tesisi ayrı toz siloları, düz ve eğimli agrega kayışları ve astarlı agrega tutma haznesini birleştirir. Her düzenlemenin kendi denetim erişimine ve servis planına ihtiyacı vardır.
Bu kılavuz, harmanlama tesisi bakımını seçtiğiniz ekipmana bağlar: neyin denetleneceği, işin nasıl organize edileceği ve bir beton tesisini onaylamadan önce hangi bakım hükümlerinin onaylanacağı.
İçindekiler Tablosu
Santral Bakım Neleri Kapsamalı?
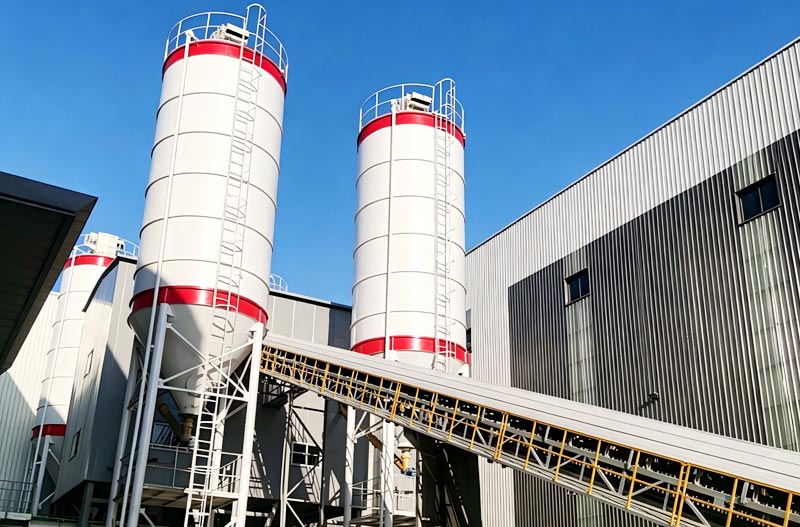
Tam bir plan, malzemeyi depolamadan deşarja kadar takip ederken aynı zamanda süreci ölçen, kontrol eden ve koruyan sistemleri de kapsar. Mikserin temizlenmesi bu planın yalnızca bir parçasıdır.
Üç sonucu ayırın: ekipman güvenli kalır, üretim fonksiyonları güvenilir kalır ve tesis belirtilen betonu teslim etmeye devam eder Tamamlanan bir onarım otomatik olarak üçünü de oluşturmaz.
Santral bakımının harmanlanması için varlık tanımlayıcıları, uygulanabilir kılavuzlar, servis sorumlulukları ve gerekli kayıtları içeren bir ekipman kaydı oluşturun Dışarıdan temin edilen ekipmanı da tanımlayın Bir kompresör, toz toplayıcı veya alıcı sistem, farklı bir yüklenicinin tedarik etmesi nedeniyle programdan kaybolmamalıdır.
Kayıt ayrıca bir sorgulamayı daha kullanışlı hale getirir.belirsiz bir şekilde “bakımı kolay” bir tesis talep etmek yerine, belirli bileşenleri, erişim gereksinimlerini ve bakım kaynaklarını tartışabilirsiniz.
Planı Bitki Konfigürasyonunuzla eşleştirin
Santral bakımı, ilgisiz bir istasyondan kopyalanan bir kontrol listesi yerine önerilen donanımı yansıtmalıdır.
Yana monteli kemer bitkileri
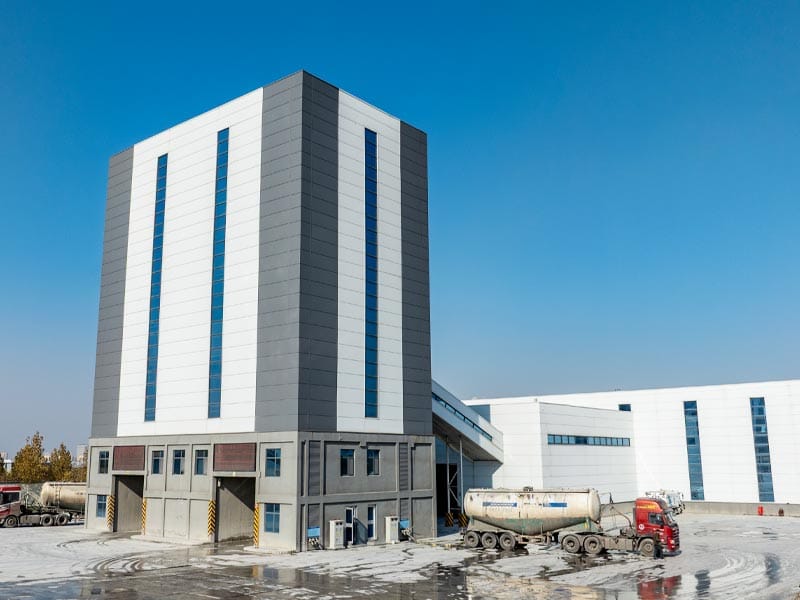
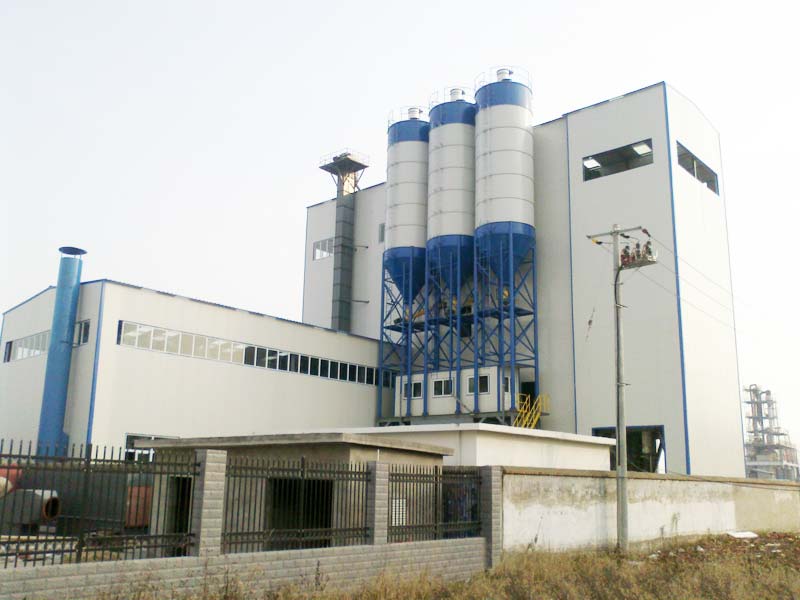
Yana monteli düzenlememizde agrega, düz ve eğimli bantlardan aşınmaya dayanıklı astarlı ve iki boşaltma kapılı geçici bir depolama haznesine geçer. Konveyör erişimini, hazne inceleme açıklıklarını ve kapı servisini ayrı görevler olarak gözden geçirin. Astarın konumu önemlidir: bir tutma-hazne astarı bir karıştırıcı astarı değildir.
Mobil bitkiler
Bizim mobil beton santrali modüler bir çerçeve ve çift şaftlı zorlamalı karıştırıcı kullanır. Yer değiştirmeden etkilenen bağlantılar ve desteklerle birlikte mikserin şaft ucu sızdırmazlık düzenlemesini servis tartışmasına dahil edin. Hareketlilik, yeniden devreye alma kontrollerini kaldırmaz.
Prefabrik bitkiler
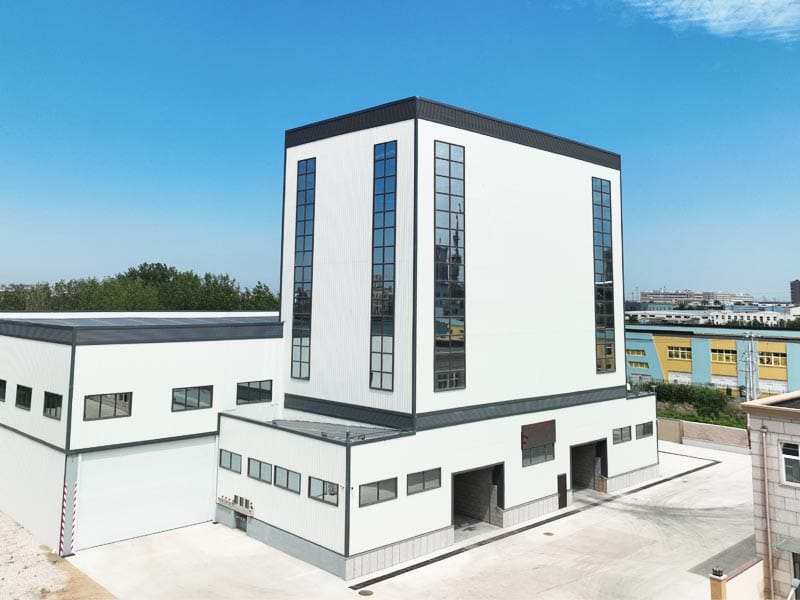
The prefabrik beton santrali planet karıştırma, çoklu boşaltma kapıları ve üretim hattı yazılım arayüzlerini kullanır. Bakım planı, yalnızca karıştırıcı sürücüsünü değil, kurulu her boşaltma rotasını ve döküm hattıyla değiştirilen sinyalleri ele almalıdır.
Pratik Bir Santral Bakım Programı Oluşturun
Aşağıdakileri modele özel kılavuzun yerine değil, bir planlama çerçevesi olarak kullanın. Gerçek aralıklar işletme görevine, ortama, denetim bulgularına ve geçerli gereksinimlere bağlıdır.
HSE'ler ekipman denetimine ilişkin rehberlik risk, üretici önerileri ve işletme deneyimi etrafında denetim kapsamı ve sıklığı ayarlamayı destekler Her harman istasyonu için tek bir evrensel program oluşturmaz.
| Planlama noktası | Organize etmek için çalışın | Yararlı kayıt |
|---|---|---|
| Her vardiyadan önce | Çözülmemiş kusurları gözden geçirin; onaylanmış kullanım öncesi gözlemleri ve güvenlik kontrollerini belirlenen konumlardan tamamlayın. | Kusurlar, işletme kısıtlamaları ve sorumlu kişi. |
| Üretimden sonra | Onaylanmış temizlik ve temizlik rutinini tamamlayın; sızıntı, kalıntı veya olağandışı aşınmayı bildirin. | Temizlik tamamlama ve olağanüstü çalışma. |
| Haftalık planlama incelemesi | Eğilimleri, parça hazırlığını ve yaklaşan çalışmaları gözden geçirin. Her hafta otomatik olarak değil, vadesi geldiğinde izole bir denetim düzenleyin. | İş emirleri, kaynaklar ve planlanan kapatma penceresi. |
| Belirtilen saatlerde veya aralıklarla | Bileşen üreticisinin yağlama, servis, muayene ve doğrulama görevlerini gerçekleştirin. | Saatler, ölçümler, takılan parçalar ve kabul sonuçları. |
| Onarım, yer değiştirme veya anormal olaylardan sonra | Hangi güvenlik, ölçüm ve üretim fonksiyonlarının serbest bırakılmadan önce yeniden incelenmesi gerektiğini belirleyin. | Etkinlik ayrıntıları, testler ve yeniden başlatma yetkisi. |
Yararlı bir harmanlama tesisi bakım kontrol listesi, her göreve bir sahip ve bir eylem eşiği verir. “Mikseri inceleyin” çok belirsizdir. “Belgelenen değiştirme kriterlerine göre astar koşulunu kaydedin” teknisyene hangi kanıtların gerekli olduğunu söyler.
Güvenli İzolasyonu İlk Gereksinim Haline G
Santral bakımı sadece bir durdurma düğmesine bağlı olmamalıdır Elektrik malzemeleri, basınçlı hizmetler, yerçekimi beslemeli malzeme ve hareketli bileşenler göreve özel izolasyon prosedürü dahilinde değerlendirmeye ihtiyaç duyar.
HSE'ler güvenli bakım rehberliği malzemeleri kilitleme, depolanan enerjiyi kontrol etme, düşebilecek parçaları destekleme ve yetkin personel kullanma adresleri. Erişim sağlamak için korumalar ve kilitlemeler atlanmamalıdır.
Müdahaleci çalışmadan önce, yetkili personel saha prosedürü kapsamında güvenli durumu oluşturmalı ve doğrulamalıdır. Karıştırıcı veya silo girişi, kapalı alan ve diğer tehlikelerin ayrı bir değerlendirmesini gerektirir; bu makale bir giriş prosedürü değildir.
Alıcılar bir izolasyon noktası çizimi ve güvenli hizmet erişiminin gösterimini talep etmelidir. Bakım ilkeleri için burada İngiliz rehberliğine atıfta bulunulmaktadır; yerel yasal gereklilikler ve kurulu ekipmanın talimatları fiili çalışmayı yönetir.
Mikser Temizliği ve Aşınma Muayenesini Ayrı Tutun
Santral bakımının harmanlanması için iki farklı görev tanımlayın: onaylanmış temizleme yöntemiyle malzemenin çıkarılması ve sonrasında bıçakların, kolların, astarların, contaların ve boşaltma bileşenlerinin durumunun değerlendirilmesi Temiz bir görünüm aşınma ölçümü değildir.
Mikser kılavuzunun muayene yerlerini, izin verilen izinleri ve değiştirme kriterlerini isteyin.Ardışık denetimler karşılaştırılabilir olacak şekilde bulguları tutarlı yerlerde kaydedin. Evrensel bir bıçak boşluğu icat etmeyin veya parçaları yalnızca çevrimiçi bir kontrol listesi bir takvim tarihi atadığı için değiştirmeyin.
Beton kalitesi bu incelemeye aittir. NIST'in beton karıştırma yöntemlerinin gözden geçirilmesi beton performansı ve homojenlik yoluyla karıştırmayı değerlendirir Önemli mikser çalışmasının ardından, sorumlu teknoloji uzmanının kabul edilebilir sonuçları doğrulamak için gereken üretim kontrollerini tanımlamasını sağlayın.
Temizleme suyu muhafazasını ve personel korumasını da planlayın. HSE'ler çimento güvenliği kılavuzu identifies dermatitis and burns from wet cement. Confirm which cleaning methods are compatible with seals, sensors and electrical enclosures before using them.
For batching plant maintenance, keep the mixer chamber and aggregate hopper on separate inspection sheets. Record part identification, installation date and the agreed condition measurements. A mixed list of “liners” can send the wrong replacement to the job. Confirm the drawing revision and mounting details before ordering replacement parts.
Agrega Konveyörleri ve Transfer Noktalarını Birlikte İnceleyin
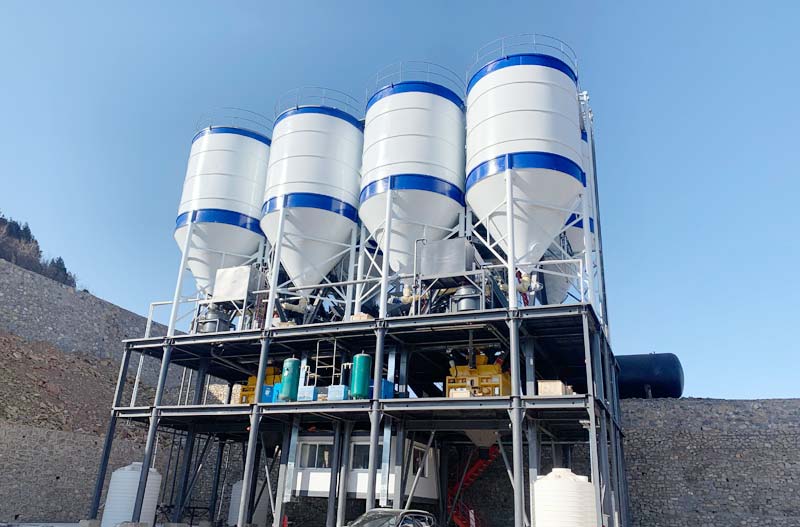
Batching plant maintenance should follow the entire aggregate route. A belt inspection and a clean floor do not explain why material repeatedly accumulates at one transfer point.
For a belt-fed installation, arrange documented checks of belt condition, tracking, rollers, transfer chutes and the receiving hopper. Separate observations permitted during normal operation from work requiring shutdown and isolation. Never reach into a moving conveyor or attempt a running adjustment from an exposed position.
Repeated spillage is a reason to investigate the loading point, material trajectory and receiving condition—not simply assign more sweeping. Record where and when it appears. Comparisons are more useful when the aggregate fraction and production setting are known.
During equipment selection, review how a technician reaches the return belt, replaces an installed roller and removes a worn hopper liner. Put the required working envelope on the general arrangement drawing.
Bakım Sonrası Tartım Doğruluğunu Koruyun
The maintenance question is whether the installed measuring system remains fit for use after service, cleaning or physical changes. Detailed tolerance selection belongs in the separate guide to batching and weighing accuracy.
Include weighing assemblies in batching plant maintenance records. Preserve unusual zero readings, mechanical-contact observations and any work on supports, connections or load cells. A repeated zero adjustment is not evidence that the underlying condition has been corrected.
NRMCA’s plant certification guidance calls for scale verification after a portable plant moves, after maintenance affecting weighing systems and when accuracy is in doubt. It also requires checks across the working range and detailed results rather than a simple acceptable/not-acceptable statement.
These are requirements within that guidance, not a claim that every plant is certified. Agree the applicable verification scope and acceptance criteria for your installation.
Silo Korumasından Ayrı Toz Çıkarma
Dust-control performance and silo protective functions need distinct entries in the batching plant maintenance plan. One inspection should not silently stand in for the other.
For extraction equipment, obtain the commissioning benchmarks, test locations and filter-service instructions. HSE’s local exhaust ventilation commissioning guidance explains how documented operating conditions and performance measurements provide a reference for later examinations.
Compare subsequent readings under comparable conditions. A running fan or a newly fitted filter does not, by itself, demonstrate adequate capture at every extraction point.
For each supplied silo, separately identify the level monitoring, venting and protective devices specified by its designer. Obtain inspection and functional-test instructions. Do not alter relief settings or bypass alarms to maintain production. Confirm the actual supply scope rather than assuming every protective feature is standard.
Yağlama, Pnömatik ve Kontrol Fonksiyonlarını Dahil Edin
A batching plant maintenance plan needs a component-specific lubrication schedule: lubricant specification, application point, quantity, interval and method. Request these from the equipment documentation instead of assigning the same grease or frequency throughout the plant.
For fitted compressed-air equipment, identify service points, drains, protection devices and operating limits. HSE’s guidance on using pressure systems emphasizes suitable maintenance, functioning protective devices and competent personnel. Apply the requirements relevant to the installed system and jurisdiction.
Control-system work needs a record too. Preserve approved settings and software versions, document changes and test the affected operating sequence. For precast production, include the receiving-station signals in that test scope.
Batching plant maintenance is incomplete when a replaced component works locally but the complete sequence has not been checked. An output indication and a confirmed mechanical response should be distinguished during the approved test.
Tekrarlanan Kusurları Belirli İş Emirlerine Dönüştürün
Useful batching plant maintenance records connect a symptom to an investigation and a verified outcome. They do not diagnose a fault solely from its appearance.
The following examples are planning prompts for qualified personnel, not instructions to operate defective equipment.
| Reported symptom | Evidence to preserve | Work-order question |
|---|---|---|
| Recurring material beneath one transfer point | Location, aggregate fraction, operating stage and photographs taken safely. | Which loading, conveying or receiving condition explains the repeat pattern? |
| Longer discharge time | Comparable batch quantities, elapsed time and relevant indications. | Is the restriction mechanical, material-related or downstream? |
| Changing scale zero | Reading history and recent cleaning or repair activity. | What inspection and verification establish the cause? |
| Extraction performance outside its agreed range | Test point, operating condition and commissioning benchmark. | What correction restores demonstrated extraction performance? |
Give each record a component identifier, owner and closure requirement. Repeat defects should remain visible until the agreed follow-up demonstrates improvement. Closing a work order because someone attended the plant is not the same as resolving it.
Sadece Onarımı Değil, Tüm Kapatmayı Planlayın
Batching plant maintenance planning should include access preparation, isolation, the repair itself, reassembly and return-to-service checks.
Consider a hypothetical task: 20 minutes to prepare and isolate, 35 minutes for the repair, 20 minutes for reassembly and inspection, and 25 minutes for controlled testing and release. If these stages are sequential, the required window is 100 minutes—not 35.
These figures are illustrative, not product service-time claims. Their purpose is to show why a spare part on the shelf does not establish how quickly production can resume.
Before scheduling batching plant maintenance, confirm parts compatibility, tools, lifting arrangements, qualified personnel and the acceptance test. Identify missing information while the work can still be planned. During equipment procurement, the same review exposes maintenance access that a compact layout may overlook.
For batching plant maintenance records, distinguish elapsed downtime from labor time. Two technicians working together for one hour contribute two labor-hours, but the plant may be unavailable for one hour rather than two. Record waiting for parts, active repair and release testing separately when reviewing where better preparation would help.
Yer Değiştirme veya Büyük Çalışmadan Sonra Tesisi Yeniden Kontrol Edin
Mobile equipment needs an event-triggered release process, not just another date on the calendar. For batching plant maintenance after relocation, identify connections, supports, guards and instruments affected by dismantling and reassembly.
HSE’s equipment inspection guidance addresses reinspection following reassembly where safety depends on installation conditions. NRMCA’s guidance separately addresses scale verification after a portable plant moves. These checks have different purposes.
Use a coordinated release record covering the affected safety functions, mechanical systems, measuring equipment and production sequence. Keep unresolved items visible and specify who can authorize restart. Factory precommissioning does not demonstrate the condition of every system after transport and installation.
Tesisi Sipariş Etmeden Önce Bakım Erişimini Belirtin
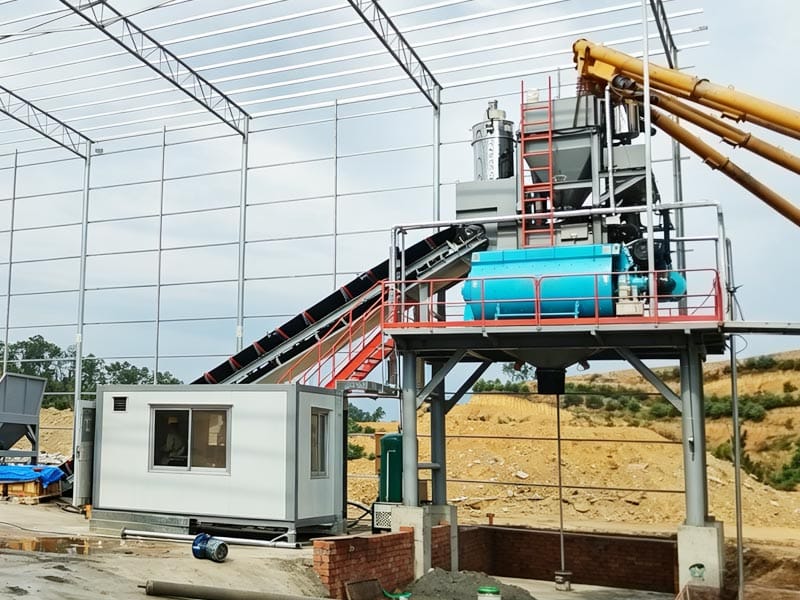
Bring batching plant maintenance into the plant layout and configuration review. Provide the operating schedule, available shutdown windows, site dimensions and the maintenance capabilities of your team.
Review component removal paths as carefully as routine inspection access. Can the proposed liner, drive or valve assembly pass through the available opening? Where will lifting equipment stand? Does the service area conflict with truck loading or aggregate deliveries?
Request a handover package containing component manuals, lubrication instructions, parts identification, relevant drawings, baseline test records and agreed training. Confirm these deliverables in the project scope.
This turns batching plant maintenance from a general promise into a set of practical design requirements. The aim is a plant your team can inspect, service and return to operation using documented methods.
Sonuç
Effective batching plant maintenance combines a realistic schedule with safe access, model-specific instructions, traceable work records and checks after intervention. The right starting point is the actual equipment configuration, not a universal list of intervals.
Share your concrete products, operating hours and site layout with our team. Request a concrete plant configuration review that includes maintenance access, service documentation and the provisions your production operation needs.
SSS
How often should batching plant maintenance be carried out?
Combine approved pre-use checks, cleaning routines, component-specific service intervals and event-triggered inspections. Use the manufacturer’s instructions and site risk assessment to set the schedule. A weekly planning review does not mean every component needs weekly servicing.
Which parts need the most maintenance attention?
Start with the fitted mixer, material-transfer equipment, discharge components, measuring systems and protective functions. Rank work by safety significance, duty and inspection history. The priorities for a belt-fed station may differ from those for a precast or frequently relocated plant.
Does a mobile plant need checks after each move?
Its release plan should address systems affected by transport and reassembly. Scale verification after relocation is specifically addressed in NRMCA’s guidance. Confirm the wider inspection and recommissioning scope with the equipment manufacturer and responsible site personnel.
Can one lubrication schedule cover every mixer?
No. Obtain instructions for the actual mixer, drive, bearings and sealing arrangement. Lubricant specifications and application requirements should come from the relevant documentation. Do not assume planetary and twin-shaft configurations use interchangeable service instructions.
What maintenance information should a plant buyer request?
Request service-access drawings, manuals, parts identification, lubrication requirements, isolation information and relevant baseline tests. Agree training and handover responsibilities. These documents help evaluate the proposed plant before maintenance constraints become operating problems.